Can MBR System Wastewater Treatment Improve Effluent Quality
Can MBR System Wastewater Treatment Improve Effluent Quality
September 21, 2026
Author
Solution Provider, through a professional technical team, we provide customers with targeted equipment selection recommendations and comprehensive after-sales services, winning the trust and recognition of customers.
Sarah M.
Hinada Water Treatment Tech Co., Ltd. (HINADA) is a leading Chinese manufacturer specializing in advanced MBR system wastewater treatment solutions. Their range includes MBR membrane bioreactor plants, membrane modules (both hollow fiber and flat sheet), compact and containerized MBR systems, and integrated UF system manufacturer expertise. HINADA’s MBR technology consistently delivers superior effluent quality, ensuring low BOD, COD, and pathogen removal, far exceeding regulatory requirements. The article explores the technical and practical advantages of HINADA’s offerings—including flexibility, operational efficiency, and minimized sludge production. HINADA’s MBR membrane modules provide a physical barrier to contaminants, making their systems ideal for municipal, industrial, decentralized, and greywater recycling applications. Buyers benefit from robust after-sales support, customization, and proven reference projects worldwide. For genuine purchasing buyers, HINADA offers reliability, technical depth, and the ability to integrate MBR and UF systems for enhanced performance. Their customer-centric approach, quality assurance, and dedication to long-term partnerships make them a top choice for organizations seeking high-effluent-quality wastewater treatment systems that deliver regulatory compliance and operational peace of mind.
Introduction to MBR System Wastewater Treatment
As sustainability and environmental protection become top priorities across industries, the demand for advanced wastewater treatment solutions is at an all-time high. The Membrane Bioreactor (MBR) system wastewater treatment has emerged as a transformative technology that meets stringent discharge standards, delivers high-quality effluent, and optimizes operational efficiency. At Hinada Water Treatment Tech Co., Ltd. (abbreviated as HINADA), we understand the global shift toward responsible water management and are committed to providing cutting-edge solutions tailored for municipal, industrial, and commercial applications.
Understanding How MBR Systems Work
An MBR system wastewater treatment process combines conventional biological treatment with advanced membrane filtration. This fusion allows HINADA’s MBR plants to efficiently separate solids and microorganisms from treated water, resulting in exceptionally clear and pathogen-free effluent. Our MBR systems utilize submerged membrane modules (membrane bioreactor modules), such as hollow fiber or flat sheet membranes, to achieve superior filtration compared to traditional methods like activated sludge.
Key Product Keywords Integrated at HINADA
MBR System Wastewater Treatment
MBR Membrane Bioreactor
MBR Membrane Module
MBR Wastewater Treatment Plant
MBR Sewage Treatment Plant
Submerged MBR System
Industrial MBR System
Municipal MBR Plant
MBR Membrane Filtration System
Flat Sheet MBR Membrane
Hollow Fiber MBR Membrane
Compact MBR System
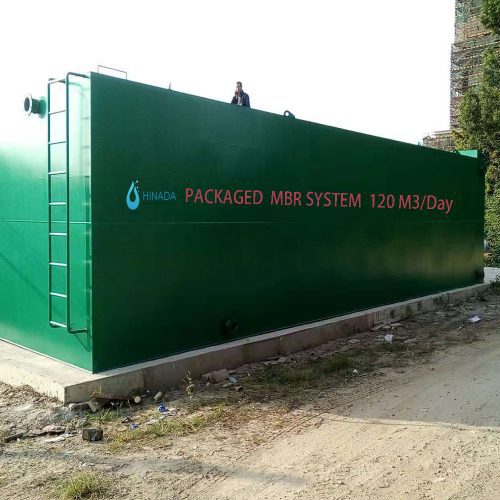
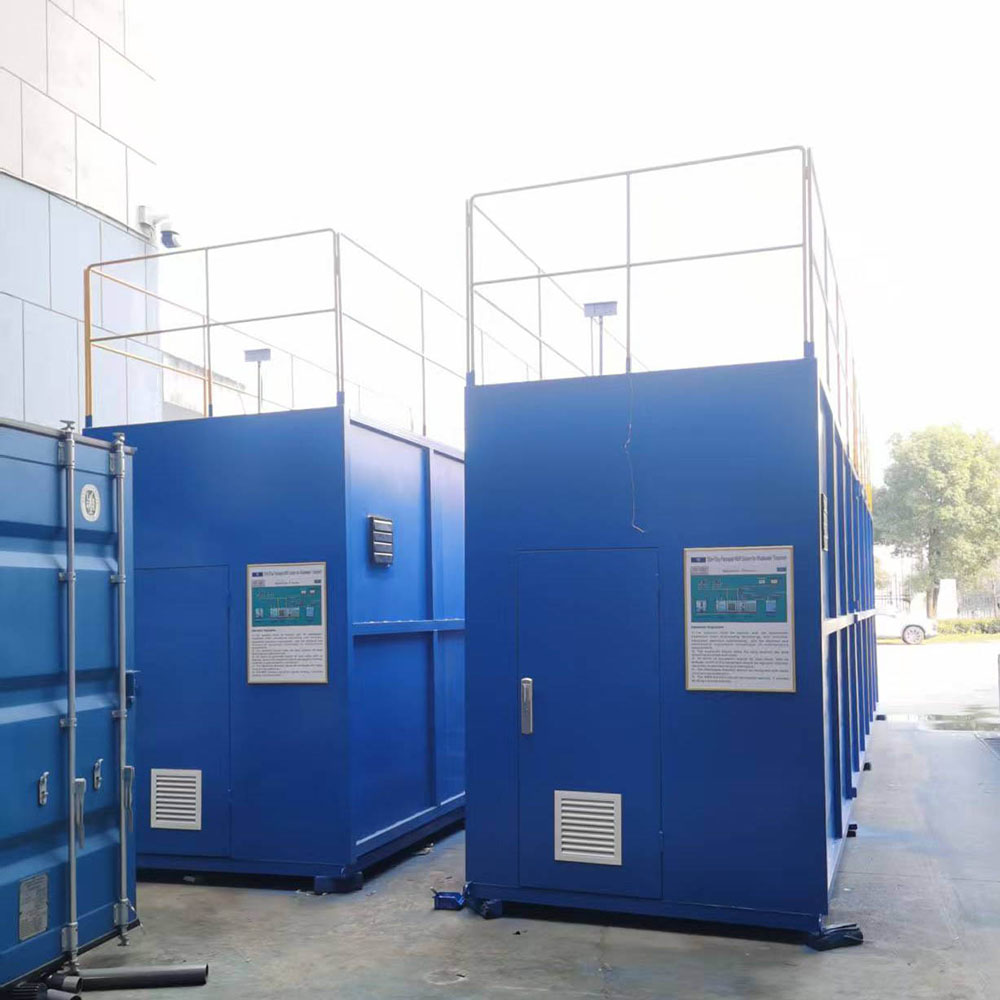
Containerized MBR System
Small Scale MBR System
Advanced MBR Wastewater Treatment Technology
MBR Effluent Quality Improvement
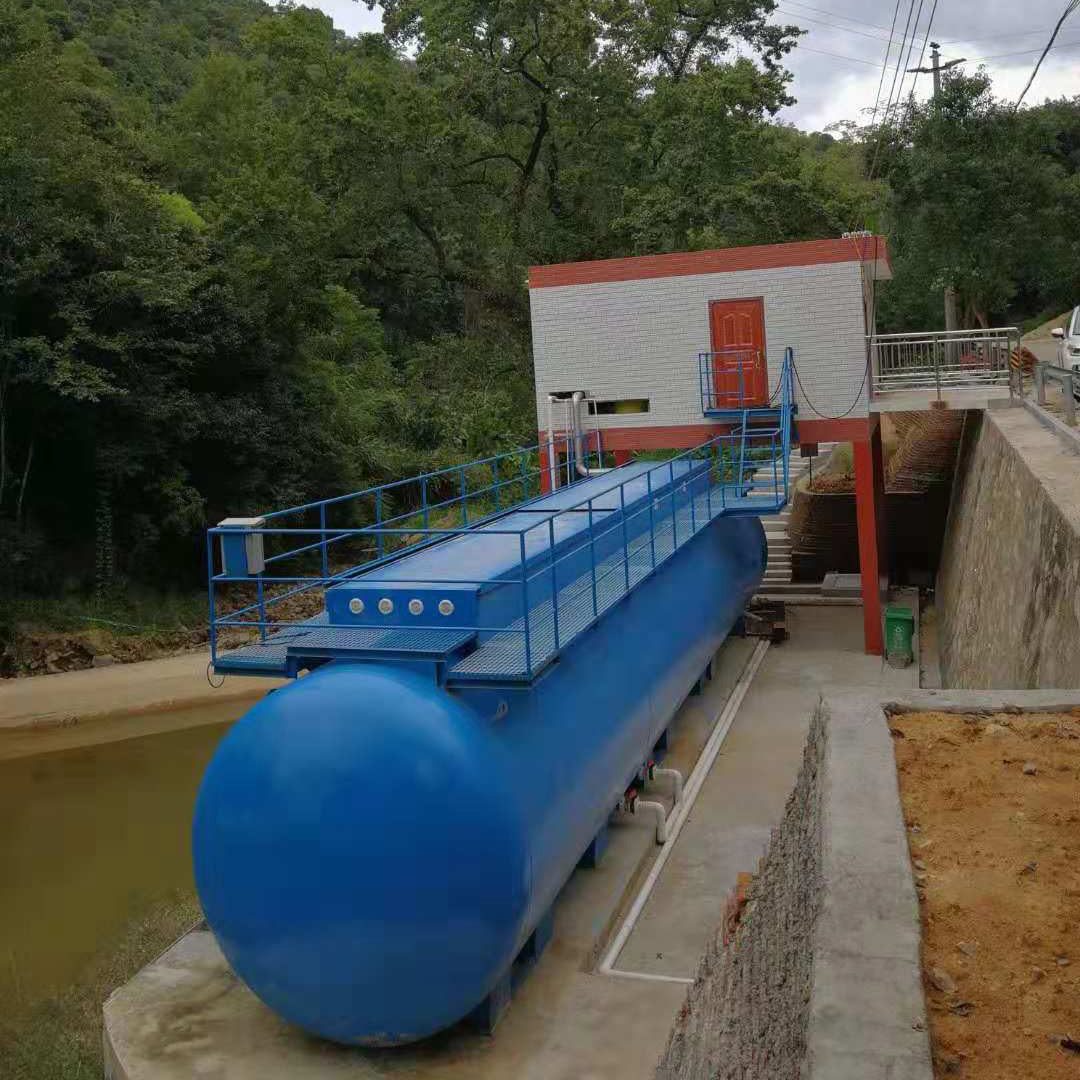
Decentralized MBR Wastewater Treatment
MBR Greywater Recycling System
MBR Sludge Reduction Solution
How MBR System Wastewater Treatment Enhances Effluent Quality
At HINADA, our MBR system wastewater treatment solutions guarantee effluent quality that surpasses regulatory requirements for BOD, COD, TSS, ammonia, and pathogens. Membrane-based separation delivers a physical barrier to bacteria and viruses, ensuring water suitable for reuse or discharge into sensitive environments. With MBR membrane bioreactor technology, our clients can achieve:
Consistently low turbidity and suspended solids
Effective removal of pathogens, bacteria, and viruses
Stable effluent quality regardless of influent fluctuations
Reduced chemical consumption
Compact footprint
Our advanced MBR membrane modules—available in both hollow fiber and flat sheet configurations—ensure robust filtration and minimal membrane fouling. HINADA’s submerged MBR systems can be adapted for industrial, municipal, and decentralized applications, ensuring versatility and scalability.
Advantages of HINADA MBR Membrane Bioreactor Systems
High-quality effluent: Our MBR wastewater treatment plants deliver effluent with <2 mg/L BOD and <1 NTU turbidity, meeting the highest reuse and discharge standards.
Flexibility and scalability: HINADA offers compact MBR systems for small-scale projects and containerized MBR systems for remote or mobile applications.
Energy and cost efficiency: Advanced aeration design and high flux membranes lower operating costs and maintenance needs.
Municipal Wastewater Treatment: Our municipal MBR plants serve large city utilities, satellite communities, and township developments with reliable effluent quality.
Industrial MBR System Wastewater Treatment: Industrial MBR systems handle complex waste streams from food processing, pharmaceuticals, textiles, and chemical manufacturing.
Decentralized and Small Scale MBR Solutions: HINADA’s compact and containerized MBR systems are ideal for hotels, resorts, office buildings, and remote communities.
Greywater Recycling: Our MBR greywater recycling systems enable commercial and residential buildings to reuse water for irrigation, flushing, or cooling.
Purchasing Psychology: Why Choose HINADA for MBR Wastewater Treatment?
Purchasing managers and professional buyers seek partners who combine technical expertise with reliability and after-sales support. At HINADA, we recognize that choosing an MBR or UF system manufacturer is not just about equipment—it’s about long-term performance, regulatory compliance, and peace of mind. Our robust quality assurance, customization options, and strong references from successful global installations position HINADA as a trusted supplier.
We provide complete design, installation, commissioning, and after-sales technical support. Our engineers help clients select the best-fit MBR membrane modules, optimize plant layout, and automate operation for minimum operator intervention. Each project benefits from our strict membrane selection process and in-house testing protocols, ensuring that every MBR membrane filtration system delivers as promised.
Technical Deep Dive: MBR Membranes and Operational Excellence
The heart of HINADA’s MBR system wastewater treatment is the membrane module. We offer both hollow fiber MBR membranes and flat sheet MBR membranes designed for high chemical resistance and longevity. Our proprietary membrane formulation and structure reduce the risk of fouling, extend cleaning intervals, and ensure stable operation even with variable feedwater quality.
Our advanced MBR membrane filtration system integrates with modern SCADA controls for real-time monitoring and automatic process optimization. This operational transparency is invaluable for procurement managers and facility operators who require consistent performance and ease of maintenance.
Integrating UF System Manufacturer and MBR System Manufacturer Expertise
As both an MBR system manufacturer and a UF system manufacturer, HINADA is uniquely positioned to offer integrated solutions for complex water treatment challenges. Ultrafiltration (UF) is often used as a pre-treatment or post-treatment step in MBR plants, ensuring even higher water quality for advanced reuse or potable applications. Our engineering team tailors each system to client requirements, leveraging the synergies between MBR and UF technologies for ultimate reliability and efficiency.
Our experience as a UF system manufacturer allows us to provide dual-membrane solutions for clients with stringent discharge or reuse goals, ensuring a one-stop solution with seamless integration and single-source responsibility.
Why Effluent Quality Matters: Value for Buyers
High effluent quality is not just a regulatory requirement; it is a strategic asset for municipalities and industries aiming at water reuse, environmental stewardship, and cost savings. HINADA’s MBR sewage treatment plant technology empowers buyers to:
Meet or exceed local discharge standards
Unlock new opportunities for effluent reuse (irrigation, cooling, process water)
Reduce liabilities and environmental footprint
Gain community and stakeholder trust through visible commitment to sustainability
Our advanced MBR wastewater treatment technology is widely referenced by industry leaders and regulatory authorities for its proven ability to consistently deliver superior effluent quality, regardless of influent variability.
MBR System Wastewater Treatment: Product Selection Guide
Product
Application
Capacity
Key Features
Compact MBR System
Hotels, small communities
5-100 m³/day
Plug-and-play, modular, low footprint
Containerized MBR System
Remote camps, emergency
20-500 m³/day
Mobile, fast deployment, robust
Industrial MBR System
Food, pharma, chemical
100-10,000 m³/day
Customizable, high TDS/TOC tolerance
Municipal MBR Plant
Cities, townships
500-100,000 m³/day
Scalable, lowest effluent values
Flat Sheet MBR Module
Retrofit, high-strength sewage
Varied
Easy maintenance, robust
Hollow Fiber MBR Membrane
New builds, large plants
Varied
High flux, chemical resistance
After-Sales Support and Quality Assurance at HINADA
Reliability is critical for buyers. HINADA stands by every MBR system wastewater treatment plant we supply, from membrane bioreactor modules to complete turnkey wastewater treatment systems. Our after-sales network includes on-site training, remote diagnostics, rapid spare parts supply, and ongoing technical assistance.
We offer extended membrane warranties and comprehensive maintenance contracts to ensure uninterrupted operation and predictable total cost of ownership. Each system is factory-tested before shipment, and our installation supervisors accompany every project until successful commissioning.
Reference Projects and Client Testimonials
HINADA has delivered MBR and UF systems to clients across Asia, Africa, the Middle East, and Europe. Our reference installations include municipal wastewater upgrades, zero-discharge industrial MBR plants, and decentralized village MBR sewage treatment systems. End-users consistently report:
Noticeable improvements in effluent clarity and odor
Stable operation with minimal disruptions
Significant reduction in chemical and sludge disposal costs
Responsive technical support throughout the equipment lifecycle
We are happy to provide reference contacts and arrange site visits upon request, so that buyers can see firsthand the advantages of partnering with HINADA.
Choosing the Right MBR System Manufacturer: The HINADA Edge
When selecting an MBR system manufacturer or UF system manufacturer, procurement professionals must evaluate technical capability, production capacity, quality assurance, and after-sales support. HINADA meets and exceeds these benchmarks with:
Modern manufacturing facilities and certified production processes
Research and development investment, driving innovation in MBR membrane bioreactor design
Comprehensive technical documentation and training for all supplied systems
Clear communication and fast response times for international buyers
With over a decade of experience, HINADA is recognized as a leading MBR system manufacturer offering true value to clients worldwide. Our focus is on long-term partnerships, not just one-time transactions.
Frequently Asked Questions (FAQ) for Buyers
1. How do MBR systems compare to conventional activated sludge plants?
MBR systems integrate biological degradation with advanced membrane filtration, resulting in higher effluent quality, smaller plant footprint, and reduced sludge production compared to conventional systems. HINADA’s MBR membrane modules act as a physical barrier to bacteria, viruses, and suspended solids, making MBR plants ideal for reuse and sensitive discharge applications.
2. Can HINADA’s MBR plants be customized to specific project needs?
Absolutely. We offer tailored MBR solutions for each application, including compact MBR systems, containerized MBR systems, and large municipal MBR wastewater treatment plants. Our engineering team works directly with buyers to ensure all technical and site-specific requirements are addressed.
3. What is the expected membrane lifespan?
With proper operation and maintenance, our MBR membranes typically last 5-8 years. HINADA provides comprehensive training and support to maximize membrane life in all membrane bioreactor modules.
4. How does HINADA support international buyers?
We provide English-language technical documentation, remote commissioning support, and global logistics. Our after-sales team is available for troubleshooting, spare parts, and routine maintenance wherever your project is located.
Conclusion: Invest in Superior Effluent Quality with HINADA MBR Systems
MBR system wastewater treatment is the future of advanced water management. With rising environmental standards and increasing water scarcity, buyers need reliable, cost-effective solutions that deliver the highest effluent quality. HINADA Water Treatment Tech Co., Ltd. stands ready as your trusted MBR system manufacturer and UF system manufacturer, supplying robust, proven, and efficient solutions for any scale or application.
Contact our team today to discuss your project requirements, receive a customized technical proposal, and discover how HINADA’s MBR membrane bioreactor technology can help you achieve your water treatment goals.