Is Biological Processing the Future of Food Wastewater Treatment
Is Biological Processing the Future of Food Wastewater Treatment
November 17, 2026
Author
Solution Provider, through a professional technical team, we provide customers with targeted equipment selection recommendations and comprehensive after-sales services, winning the trust and recognition of customers.
Sarah M.
This article presents HINADA Water Treatment Tech Co., Ltd. (HINADA) as a leading Chinese manufacturer of advanced biological wastewater treatment systems for the food industry. Addressing the complexities of food effluent treatment, HINADA delivers innovative solutions such as membrane bioreactor (MBR) systems, compact sewage treatment plants, high-efficiency water purification, and integrated automatic control systems. The biological processing approach, featuring aerobic digestion and sludge reduction, is highlighted as the future of food wastewater treatment, offering adaptability, operational cost savings, and compliance with stringent regulations. HINADA’s systems are engineered for scalability, ease of maintenance, and water reuse, facilitating sustainable water management and supporting buyers’ sustainability goals. With a focus on genuine buyer needs, HINADA provides custom engineered solutions, modular water treatment plants, and comprehensive technical support, ensuring a rapid return on investment and operational excellence. The article is written from the perspective of professional technical personnel and experienced procurement specialists, emphasizing the advantages of biological wastewater treatment and HINADA’s commitment to quality, partnership, and innovation. Buyers seeking reliable, cost-effective, and future-proof food wastewater treatment will find HINADA’s offerings uniquely suited to their requirements.
Is Biological Processing the Future of Food Wastewater Treatment? - HINADA's Advanced Solutions
Introduction: The Challenge of Food Wastewater Treatment
Industrial food processing generates vast volumes of wastewater, posing major challenges to environmental compliance and operational efficiency. For buyers seeking reliable, scalable solutions, the choice of food wastewater treatment technology is crucial. HINADA Water Treatment Tech Co., Ltd. (abbreviated as HINADA) is a leading Chinese manufacturer specializing in biological processing systems designed to address the unique demands of food industry effluent management. As global regulations tighten and sustainability becomes a core priority, buyers are increasingly turning to advanced biological processing methods for food wastewater treatment. This article explores the key product keywords—membrane bioreactor, food industry wastewater treatment, biological wastewater treatment, food effluent treatment, industrial wastewater treatment equipment, compact sewage treatment plant, MBR wastewater treatment system, industrial sewage treatment, high-efficiency water purification, sludge reduction, aerobic digestion, filtration units, integrated water treatment systems, automatic control system, odor removal, modular water treatment plant, custom engineered solutions, cost-effective wastewater treatment, and sustainable water management—as they relate to HINADA’s offerings.
Overview of HINADA Water Treatment Technologies
HINADA has built its reputation on innovation, quality, and tailored engineering. Our full suite of solutions incorporates membrane bioreactor (MBR) technologies, compact sewage treatment plants, high-efficiency water purification systems, and integrated automatic control systems. Every project leverages deep technical expertise and a customer-centric approach, ensuring buyers receive products engineered for their specific food effluent treatment needs. As experienced procurement professionals and technical specialists, we understand that buyers demand not only compliance, but also operational cost savings, minimal maintenance, and scalability.
Biological Wastewater Treatment: The Leading Solution
Biological wastewater treatment—especially aerobic digestion processes—is increasingly recognized as the most promising method for food industry wastewater treatment. HINADA’s proprietary MBR wastewater treatment system uses advanced filtration units and modular water treatment plant designs to deliver reliable sludge reduction and odor removal. Our custom engineered solutions are designed for seamless integration with existing industrial sewage treatment infrastructure, offering buyers the flexibility to expand or upgrade as needed. Biological processing is preferred for its ability to handle high organic loads and fluctuating influent quality, making it ideal for food processing plants, slaughterhouses, breweries, dairies, and confectionery manufacturers.
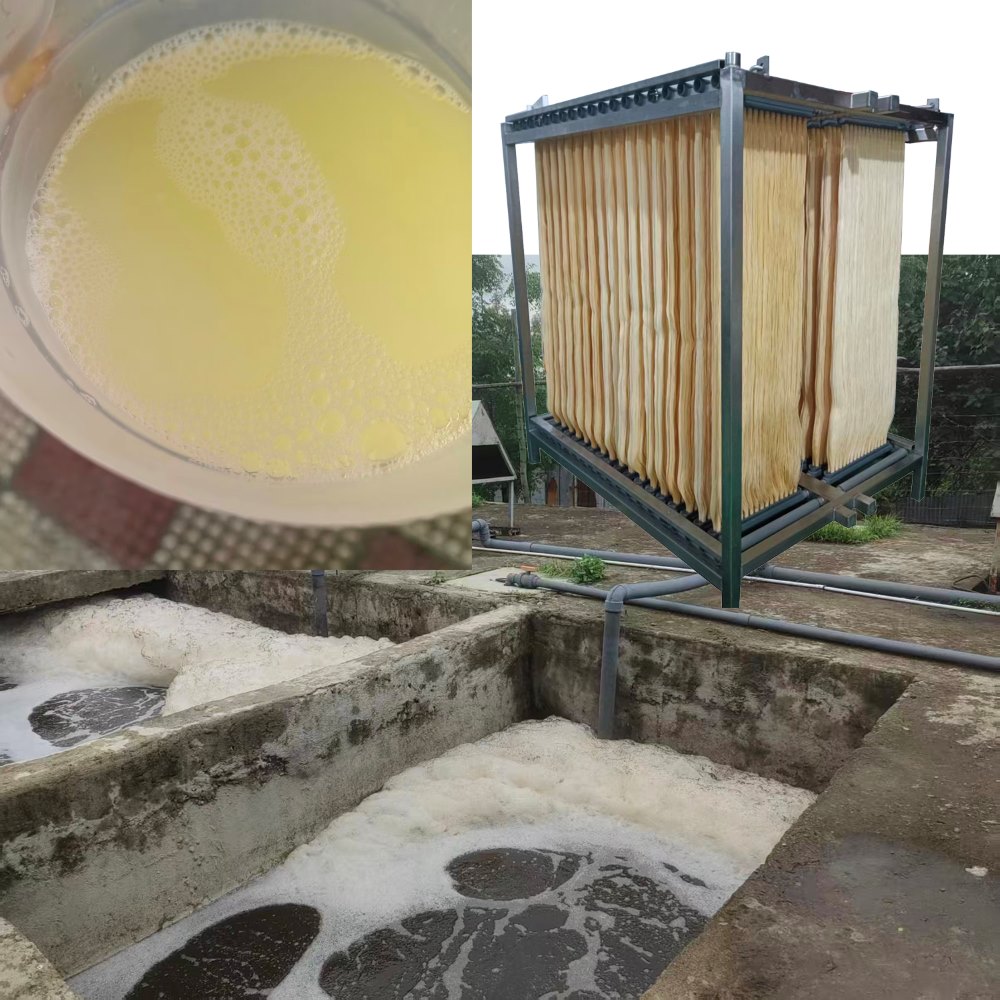
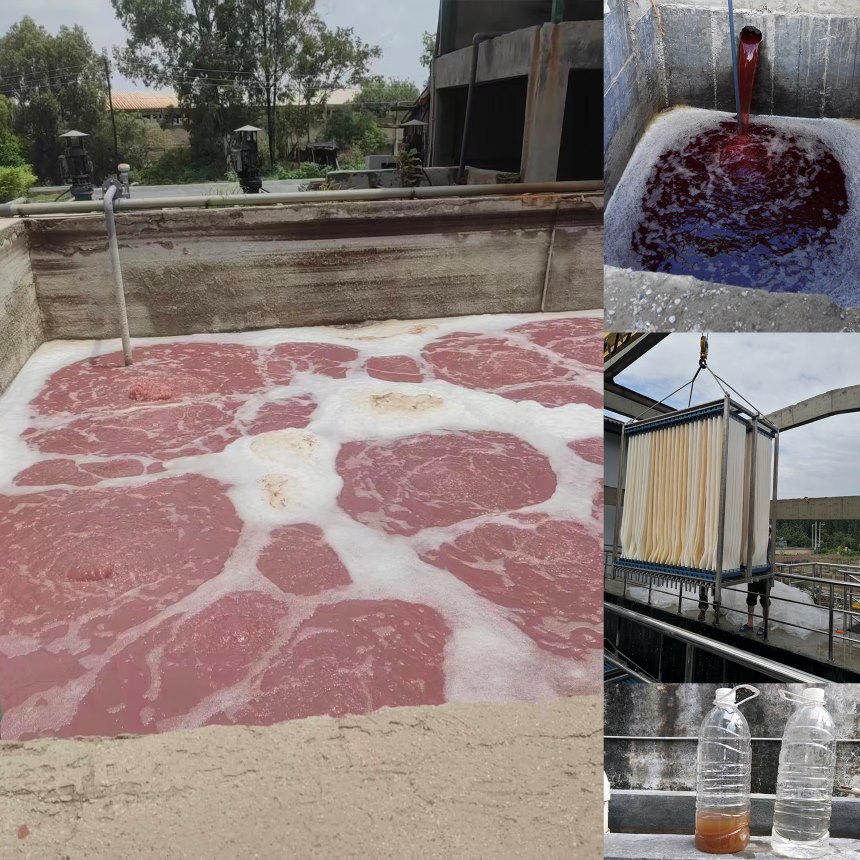
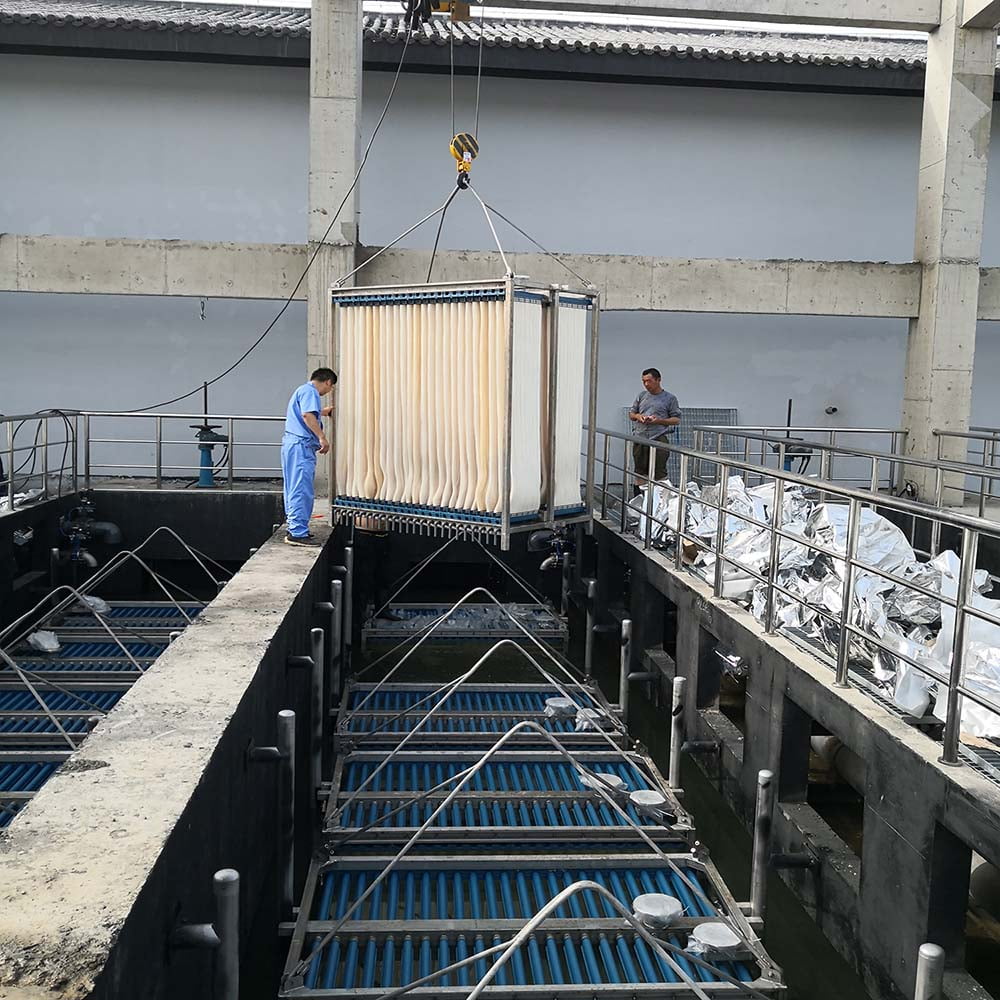
Membrane Bioreactor: HINADA’s MBR systems combine biological treatment and solid-liquid separation in a single unit, delivering superior effluent quality and reducing footprint. Our advanced membrane modules are engineered for durability and high flux, minimizing downtime and maintenance costs for buyers.
Compact Sewage Treatment Plant: Designed for rapid deployment and easy operation, these units are ideal for food factories with limited space or remote locations. The modular design allows buyers to scale up capacity as production grows.
Filtration Units: Our filtration units employ precision-engineered membranes to remove suspended solids, bacteria, and other contaminants, ensuring compliance with discharge standards and water reuse requirements.
Automatic Control System: HINADA’s integrated control systems allow buyers to monitor and optimize every stage of the food effluent treatment process remotely, reducing labor costs and minimizing human error.
Odor Removal: Advanced aeration and biofiltration modules eliminate unpleasant odors, a critical concern for food processing operations and their neighbors.
Integrated Water Treatment Systems for Sustainable Water Management
HINADA’s integrated water treatment systems are designed for sustainable water management and maximum resource recovery. By combining biological wastewater treatment with advanced membrane filtration, our solutions enable the reuse of treated water for cleaning, cooling, and even process applications. This not only reduces operational costs but also supports environmental stewardship, a key concern for buyers seeking to enhance their corporate sustainability profiles. Our systems are compatible with various industrial wastewater treatment equipment, making integration simple for procurement professionals.
Custom Engineered Solutions and Modular Plant Flexibility
Each food processing plant presents unique challenges—whether it’s fluctuating loads, high grease content, or strict discharge limits. HINADA offers custom engineered solutions tailored to buyer requirements, from modular water treatment plant configurations to specialized MBR membrane selection. Our modular approach allows buyers to expand capacity as needed, ensuring investment flexibility and future-proofing against production growth or regulatory changes. As a manufacturer and supplier, HINADA provides comprehensive technical support, ensuring buyers achieve optimal performance and compliance.
Cost-Effective Wastewater Treatment: Maximizing Buyer ROI
Buyers are increasingly focused on total lifecycle costs, not just upfront purchase price. HINADA’s systems are engineered for low energy consumption, minimal chemical usage, and simplified maintenance. Our automatic control systems reduce labor requirements, while high-efficiency water purification modules limit sludge generation and disposal costs. The result is a cost-effective Wastewater Treatment Solution that delivers rapid ROI for buyers. Technical personnel and procurement specialists appreciate HINADA’s transparent pricing and robust support infrastructure, making us a preferred partner for food industry wastewater treatment projects.
Sludge Reduction and Aerobic Digestion: Minimizing Operational Burdens
Sludge management is a major pain point for buyers in the food industry. HINADA’s biological wastewater treatment systems incorporate aerobic digestion processes that significantly reduce sludge volume and stabilize residues, simplifying disposal and lowering total costs. Our MBR wastewater treatment system achieves high rates of organic degradation, ensuring minimal residuals and easy handling. Buyers benefit from reduced hauling, less frequent maintenance, and consistent compliance with environmental regulations.
HINADA has delivered successful projects across Asia, Africa, the Middle East, and Europe, supplying industrial wastewater treatment equipment to food factories of all sizes. Our compact sewage treatment plants and integrated water treatment systems have enabled clients to achieve strict discharge compliance, expand production, and win sustainability awards. Buyers value our technical guidance, rapid delivery, and post-installation support, making HINADA a trusted partner for food effluent treatment.
Industrial Wastewater Treatment Equipment: Built for Reliability and Performance
HINADA’s equipment is manufactured under stringent quality controls, using corrosion-resistant materials and advanced automation. Our industrial sewage treatment products are designed for continuous operation, even under challenging conditions. Technical personnel appreciate the modularity and ease of maintenance, while procurement professionals benefit from competitive pricing and flexible delivery options. Each unit is backed by comprehensive warranties and remote technical support, ensuring buyers can operate with confidence.
High-Efficiency Water Purification and Odor Removal: Protecting Brand and Environment
For food processors, reputation and compliance are paramount. HINADA’s high-efficiency water purification solutions ensure effluent meets national and international standards. Our odor removal modules protect the surrounding community, allowing buyers to maintain positive relationships with local stakeholders and regulators. Technical personnel can easily upgrade or retrofit existing systems, thanks to our modular designs and broad compatibility with other industrial wastewater treatment equipment.
Automatic Control System: Reducing Labor and Human Error
Operational simplicity is a major purchasing driver. HINADA’s automatic control system allows buyers to manage all aspects of the wastewater treatment process from a central interface. Remote monitoring, real-time alerts, and smart optimization algorithms reduce labor requirements and minimize risk. Procurement professionals value the ability to scale and adapt control systems to changing production needs or regulatory demands.
Filtration Units and Sustainable Water Management: Supporting Circular Economy
The trend toward sustainable water management and circular economy principles is driving buyers to seek systems that enable water reuse and minimize waste. HINADA’s filtration units deliver high purity, supporting reuse in cleaning, cooling, and other non-potable applications. Our integrated water treatment systems are engineered for maximum resource recovery, helping buyers achieve their sustainability targets and improve operational efficiency.
Modular Water Treatment Plant and Custom Engineered Solutions: Flexible for Any Scale
Whether buyers operate a small food factory or a large industrial complex, HINADA’s modular water treatment plant designs allow for tailored solutions. Custom engineered solutions ensure that every aspect of the system—from membrane selection to control interfaces—matches the operational and regulatory context. Buyers can invest with confidence, knowing their system is designed for scalability and future upgrades.
Supporting Genuine Buyers: A Professional Approach from HINADA
At HINADA, we understand the purchasing psychology of genuine buyers. Our technical and procurement teams work closely with clients to identify pain points—cost, compliance, operational simplicity—then deliver solutions that address these directly. As a Chinese manufacturer with global reach, we offer transparent communication, detailed technical documentation, and rapid-response support. Buyers receive end-to-end service, from initial consultation through installation and ongoing maintenance. Our focus is on building lasting partnerships, not simply selling equipment.
Key Advantages: Why Choose HINADA for Food Wastewater Treatment?
Proven performance in biological wastewater treatment and food effluent treatment
Modular water treatment plant designs for scalability
Automatic control system for operational simplicity
Custom engineered solutions for unique buyer requirements
Cost-effective wastewater treatment, maximizing buyer ROI
Rigorous quality control and after-sales support
Emerging Trends: Sludge Reduction and Industrial Wastewater Treatment Equipment
As regulations continue to evolve and buyers seek new ways to minimize environmental impact, sludge reduction technologies and advanced industrial wastewater treatment equipment are gaining prominence. HINADA’s systems are designed to adapt to these trends, offering buyers the flexibility to upgrade and stay ahead of the curve. Our aerobic digestion modules and compact sewage treatment plants are particularly valued for their low operational costs and ease of compliance.
Conclusion: Biological Processing as the Future of Food Wastewater Treatment
Biological processing, powered by advanced membrane bioreactor technologies and integrated system controls, has emerged as the future of food wastewater treatment. HINADA’s commitment to technical innovation, customer partnership, and sustainable water management makes us the ideal supplier for buyers seeking reliable, cost-effective, high-performance solutions. Our deep understanding of buyer psychology and industry requirements ensures every project delivers real value—not just compliance, but operational excellence, resource efficiency, and brand protection.
Contact HINADA: Partner for Genuine Solutions
Ready to invest in food wastewater treatment technology that delivers lasting results? Contact HINADA Water Treatment Tech Co., Ltd. today for a personalized consultation and discover why leading buyers trust us for their biological wastewater treatment needs. Our technical and procurement teams are ready to support your next project with custom engineered solutions, modular water treatment plant designs, and ongoing technical support. Experience the HINADA difference—where expertise meets innovation, and buyers become partners in sustainable success.