Containerized MBR System Design for Compact Footprints
Containerized MBR System Design for Compact Footprints
September 29, 2026
Author
Solution Provider, through a professional technical team, we provide customers with targeted equipment selection recommendations and comprehensive after-sales services, winning the trust and recognition of customers.
Sarah M.
Hinada Water Treatment Tech Co., Ltd. (HINADA) leads the market in containerized MBR system design for compact footprints, offering advanced, modular, and portable MBR (Membrane Bioreactor) wastewater treatment solutions for municipal, industrial, and remote applications. These systems are engineered for rapid deployment, minimal site footprint, and plug-and-play operation—addressing the real needs of procurement professionals and technical buyers seeking regulatory compliance, operational reliability, and future scalability. With integrated features such as advanced MBR technology, automated controls, energy-efficient operation, and robust ISO containerized structures, HINADA’s solutions guarantee high effluent quality and operational cost savings. Our products are ideal for decentralized sewage treatment, municipal and industrial wastewater, and decentralized water reuse, including containerized greywater recycling. As a trusted Chinese manufacturer, HINADA offers customization, competitive pricing, comprehensive after-sales support, and a proven track record. Choose HINADA for your next containerized MBR project and experience best-in-class engineering, fast delivery, and long-term value.
Introduction to Containerized MBR Systems for Modern Water and Wastewater Management
In today’s rapidly urbanizing and industrializing world, the demand for advanced, efficient, and compact water and wastewater treatment solutions is growing at an unprecedented pace. Hinada Water Treatment Tech Co., Ltd., also known as HINADA, stands at the forefront of this evolution, offering technologically advanced containerized MBR system designs for compact footprints. HINADA’s innovative product range includes containerized MBR systems, integrated MBR systems, modular MBR units, portable MBR treatment plants, compact MBR wastewater systems, mobile MBR solutions, and plug-and-play membrane bioreactor (MBR) plants, specifically tailored for industries and municipalities seeking reliable, space-saving, and cost-effective treatment processes.
Understanding the Demand: Why Buyers Choose Containerized MBR Solutions
Purchasing decisions for wastewater treatment equipment are driven by crucial factors: space efficiency, treatment reliability, rapid deployment, regulatory compliance, scalability, and total cost of ownership. HINADA recognizes that buyers are not just looking for a product—they are investing in operational peace of mind, long-term value, and technical support. Whether you are a procurement officer, engineering consultant, or facility manager, the choice of a containerized MBR system must address your needs for modular wastewater treatment plants, compact MBR systems, decentralized sewage treatment, containerized MBR wastewater plants, and mobile water purification units. Proven performance, ease of transport and installation, and after-sales support are non-negotiable priorities.
Hinada’s Technical Leadership in Containerized MBR System Engineering
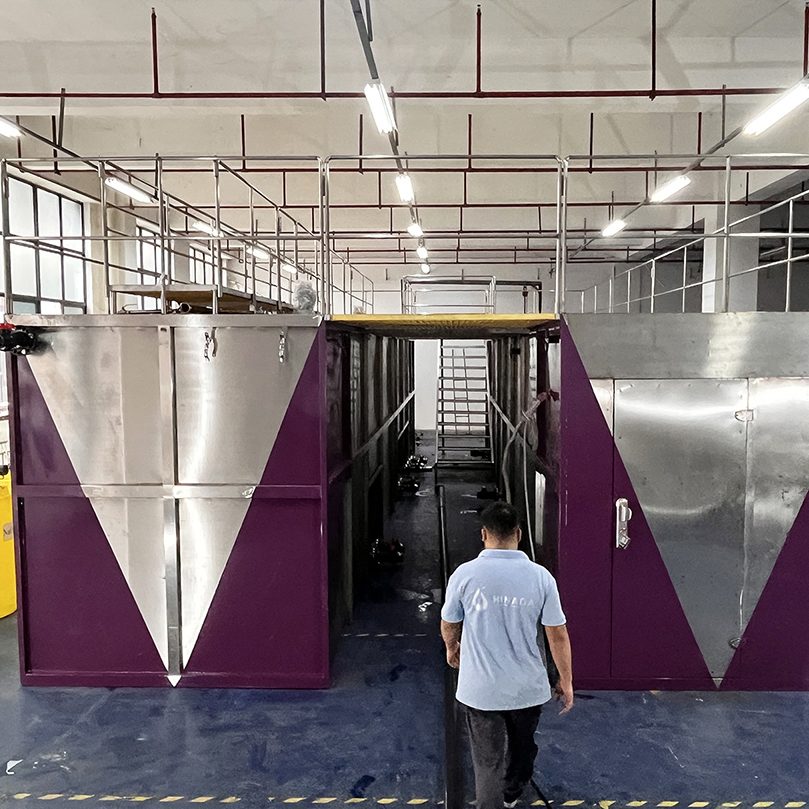
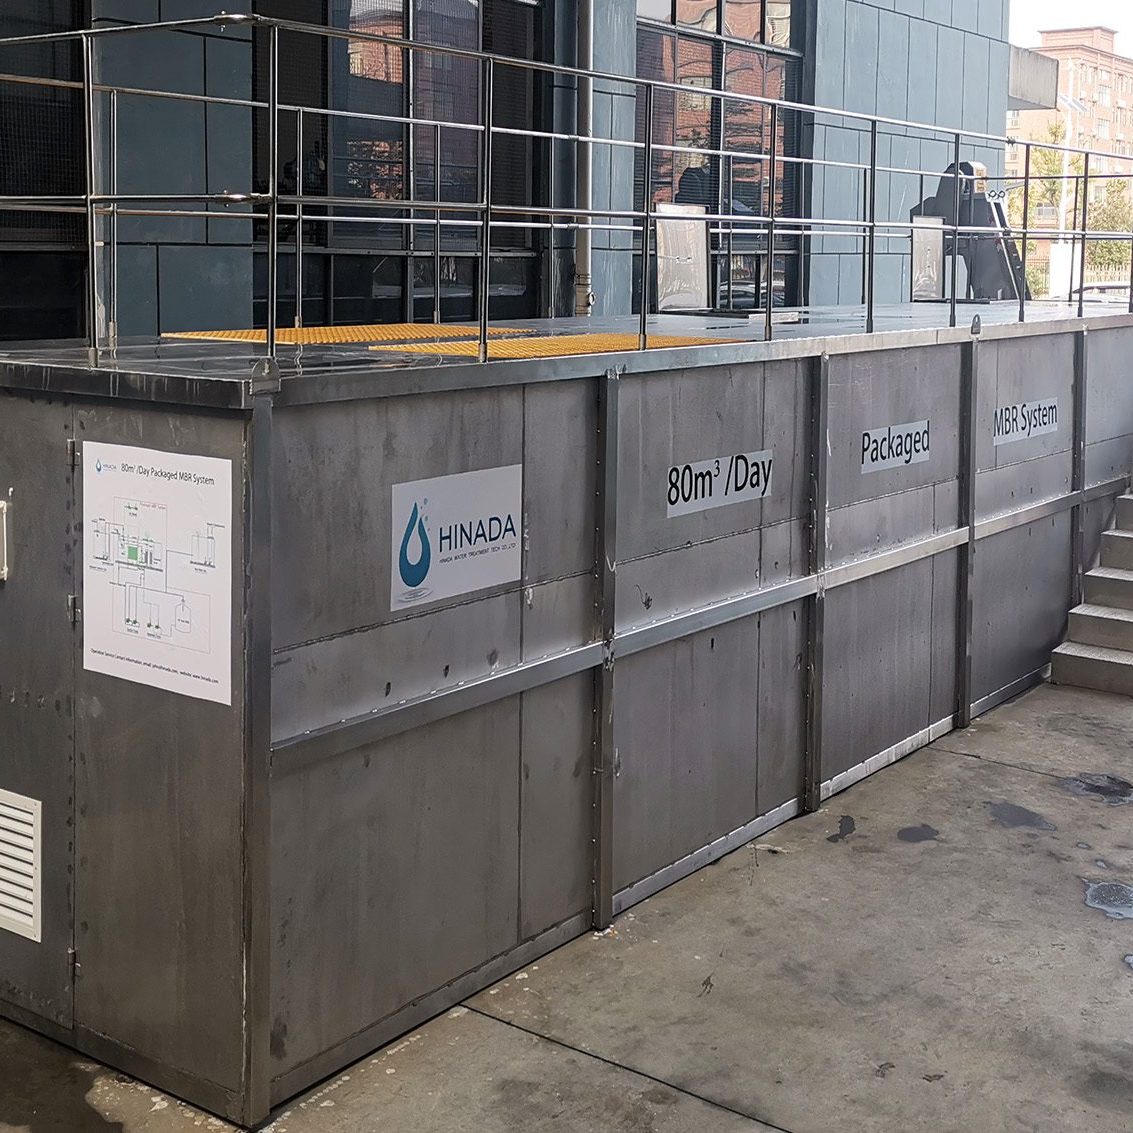
Compact Design: HINADA’s containerized MBR plants are engineered for minimal footprints, allowing installation in restricted urban or remote locations. Their modular architecture supports easy scalability, whether starting from a small portable MBR system or expanding to a large decentralized water reuse facility.
Integrated Functions: Each system integrates advanced MBR technology, automatic controls, and auxiliary equipment within standard ISO shipping containers, ensuring seamless plug-and-play operation, maximized membrane efficiency, and minimized labor requirements.
Superior Membrane Bioreactor Technology: Utilizing high-quality MBR membranes, the systems deliver exceptional effluent quality for direct discharge, reuse, or further tertiary treatment. This ensures compliance with stringent discharge and water reuse standards—crucial for buyers facing regulatory audits or supply chain requirements.
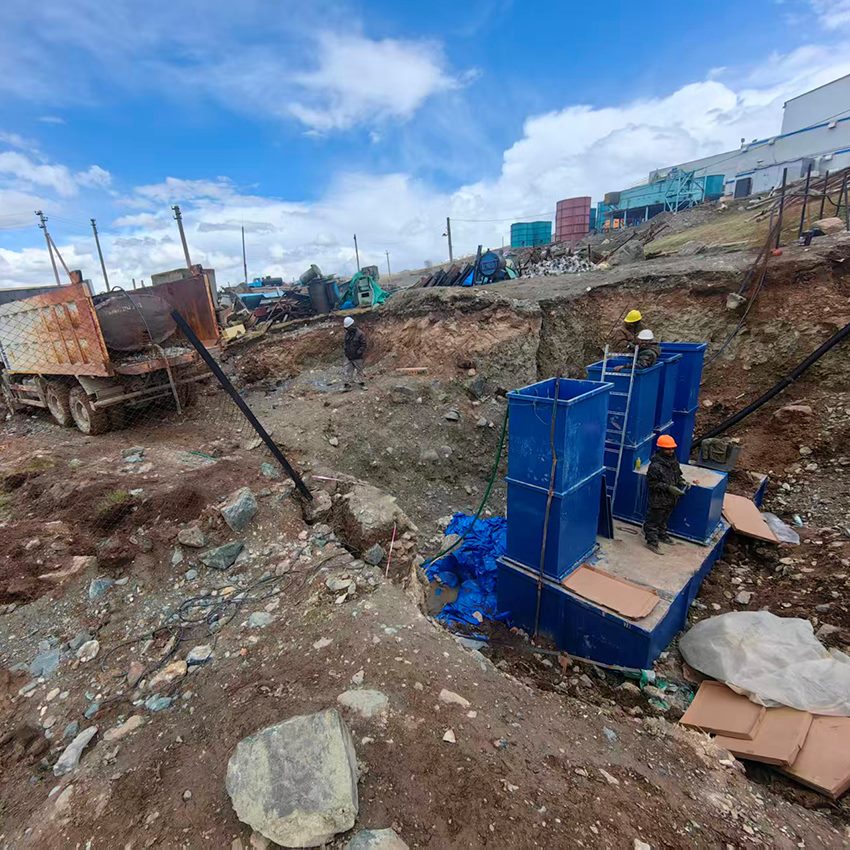
Durability and Mobility: HINADA’s containerized MBR solutions are robust enough to withstand harsh environments and frequent relocations, making them ideal for construction sites, mining camps, temporary settlements, and emergency response applications.
Key Product Advantages: Why HINADA is the Smart Buy
Fast Delivery and Setup: Pre-engineered and factory-tested, each unit is ready for rapid deployment—cutting lead times, civil construction, and site disruptions to a minimum.
Plug-and-Play Operation: User-friendly interfaces and fully integrated automation allow quick start-up and minimal operator training, reducing the need for specialized local staff.
Reliable Performance: High-quality materials and proven process flows ensure stable biological treatment, robust membrane operation, and low maintenance requirements.
Operational Cost Savings: Energy-efficient design, compact layouts, and reduced manual intervention all translate into significant cost advantages over traditional activated sludge or SBR systems.
Versatility: HINADA’s containerized MBR plants accommodate a wide range of applications—from municipal and decentralized sanitation to high-strength industrial wastewater and remote/semi-permanent installations.
Deep Dive: How HINADA Satisfies Procurement and Technical Demands
From a procurement standpoint, buyers demand transparency, proven references, and demonstrable value. HINADA addresses this by offering detailed technical documentation, international project portfolios, and flexible configuration options for containerized MBR modular design and MBR packaged wastewater treatment plants. Our professional sales and engineering teams ensure that every proposal is tailored to the site’s hydraulic, organic, and environmental requirements. We provide comprehensive cost-benefit analysis, lifecycle maintenance plans, and full compliance with ISO and CE certifications.
Technically, HINADA’s containerized MBR systems leverage advanced air scouring, automatic backwashing, and remote monitoring to guarantee continuous operation and membrane longevity. Modular expansion is straightforward—simply add more container units in parallel, with no complex civil works or process redesign, making us a preferred partner for phased or uncertain facility development.
Integrated Features: Elevating the Standard for Containerized MBR Plants
Feature
Benefit
Advanced Membrane Bioreactor (MBR) Technology
High-quality effluent, suitable for reuse and regulatory compliance
ISO Containerized Enclosure
Easy transport, fast installation, minimal site footprint
Applications: Real-World Solutions with Containerized MBR Systems
Municipal Decentralized Sewage Treatment: Perfect for small towns, villages, resorts, and new developments requiring rapid and reliable sanitation infrastructure.
Industrial Wastewater Treatment: Suitable for food and beverage, pharmaceutical, chemical, textile, and electronics industries where high-strength wastewater demands robust treatment.
Construction and Mining Camps: Mobile, easy-to-relocate solutions ensure environmental compliance and worker welfare.
Emergency and Disaster Response: Ready-to-deploy units restore sanitation rapidly in natural disasters or crisis zones.
Remote and Island Installations: Containerized form factor ensures access to clean water where traditional infrastructure is infeasible.
Why Choose HINADA for Your Containerized MBR Needs?
As a leading Chinese manufacturer, HINADA offers tangible advantages to international buyers:
Competitive Pricing: Factory-direct supply ensures cost-effective solutions without sacrificing quality.
Customization: We configure every system to your capacity, influent characteristics, and site restrictions.
Global Service: Fast delivery, worldwide technical support, and extensive after-sales service.
Quality Assurance: All systems are strictly tested under international standards and come with robust warranties.
References and Track Record: Hundreds of successful containerized MBR installations across urban, industrial, and remote settings worldwide.
Project Case: Modular Containerized MBR for an Urban Redevelopment
One of HINADA’s flagship projects involved supplying a multi-container MBR plant to a rapidly developing urban district. The client sought a compact, modular wastewater treatment solution that could adapt to changing capacity requirements over time. HINADA delivered a fully integrated plug-and-play containerized MBR system, achieving effluent quality suitable for landscaping and irrigation reuse. The installation was completed in under 10 days with no major infrastructure changes, demonstrating the superior deployment speed and scalability of HINADA’s modular MBR systems.
Special Focus: Containerized Greywater Recycling and Decentralized Water Reuse
Modern real estate and commercial projects are increasingly integrating containerized greywater recycling systems to achieve sustainability and water conservation targets. HINADA’s advanced containerized MBR systems are perfectly suited for decentralized water reuse, offering turnkey solutions for residential, hotel, and commercial complexes looking to treat and recycle greywater streams for non-potable uses. This not only reduces overall water consumption but also minimizes environmental impact and operational costs.
Customer Support and After-Sales Service: The HINADA Commitment
When buyers choose a HINADA containerized MBR system, they gain access to a comprehensive support ecosystem, including remote monitoring, regular membrane integrity checks, operator training, and prompt supply of genuine spare parts. Our team of seasoned engineers and local partners ensures that every system operates at peak efficiency throughout its lifecycle.
How to Specify the Ideal HINADA Containerized MBR Solution for Your Project
To ensure the best fit for your application, HINADA provides detailed questionnaires and technical guidance during the specification process. Key factors include:
Daily treatment capacity requirements
Influent water quality parameters (COD, BOD, TSS, ammonia, etc.)
Effluent quality targets
Site constraints (space, utilities, climate)
Preferred delivery and installation timelines
Our technical team prepares 3D drawings, process flow diagrams, and customized proposals to ensure transparency and alignment with your project goals and regulatory framework.
Environmental Impact and Regulatory Compliance
HINADA’s containerized MBR systems meet or exceed international discharge and water reuse standards (e.g., EU/US EPA, China GB), minimize sludge production, and support sustainable water management. With increasing regulatory scrutiny on wastewater discharge, investing in HINADA’s advanced solutions guarantees both environmental responsibility and future-proof compliance.
Industry Trends: The Shift Towards Decentralized, Containerized MBR Plants
Global trends point toward decentralized and containerized MBR plant adoption for both new and retrofit projects. The benefits of factory-built, rapidly deployable, and scalable water treatment are increasingly valued by developers, municipalities, and industrial operators worldwide. With rising urban densities and stricter environmental standards, the time for containerized, modular, and compact MBR systems is now—and HINADA is your trusted partner for these solutions.
Conclusion: Partner with HINADA for Future-Ready Containerized MBR System Design
Choosing HINADA means investing in world-class engineering, operational reliability, and unwavering customer support. Our containerized MBR system design for compact footprints not only addresses your immediate treatment needs but also delivers flexibility and scalability for future growth. Whether you require a standard plug-and-play unit or a fully customized modular solution, HINADA delivers unmatched value, quality, and peace of mind.
Contact HINADA Water Treatment Tech Co., Ltd. today to discuss your next containerized MBR project and discover why buyers worldwide trust us for mission-critical water and wastewater treatment solutions.