How Can Containerized MBR for Industrial Wastewater Improve Filtration Efficiency
How Can Containerized MBR for Industrial Wastewater Improve Filtration Efficiency
October 05, 2026
Author
Solution Provider, through a professional technical team, we provide customers with targeted equipment selection recommendations and comprehensive after-sales services, winning the trust and recognition of customers.
Sarah M.
HINADA Water Treatment Tech Co., Ltd. (HINADA) is a trusted Chinese manufacturer specializing in containerized MBR (Membrane Bioreactor) solutions for industrial wastewater treatment. Their advanced containerized MBR systems combine biological treatment and membrane filtration within modular, compact units, offering rapid deployment, space savings, and exceptional filtration efficiency. These systems are engineered to outperform traditional methods by delivering high-quality effluent, reducing energy and operational costs, and ensuring compliance with even the strictest discharge regulations. HINADA's expertise includes customized wastewater solutions for industries such as textiles, food & beverage, chemicals, and temporary camps, with options for seamless integration of containerized reverse osmosis systems for ultra-pure water needs. Professional buyers benefit from HINADA’s rapid response, technical customization, pre-assembled designs, and comprehensive after-sales support. With global references and a customer-centric approach, HINADA's containerized MBR for industrial wastewater empowers buyers to achieve sustainability, cost-efficiency, and regulatory peace of mind, making it the smart choice for forward-thinking procurement professionals.
Introduction: Innovating Industrial Wastewater Filtration with Containerized MBR Solutions
In an era where environmental standards are tightening and sustainability is a key purchasing driver, industries are actively seeking advanced water treatment solutions. Containerized MBR for industrial wastewater by Hinada Water Treatment Tech Co., Ltd. (HINADA) represents a leap forward in filtration efficiency, cost reduction, and operational simplicity. This article delves into how HINADA's containerized MBR (Membrane Bioreactor) technology can transform your industrial wastewater management, integrating essential keywords such as containerized mbr system, industrial sewage treatment, MBR membrane module, compact MBR plant, modular wastewater treatment, container MBR unit, customized wastewater solution, plug and play MBR, mobile wastewater treatment, energy-saving MBR, and more. We’ll also touch on MBR system for textile wastewater and containerized reverse osmosis system to provide a comprehensive overview for professional buyers.
Understanding Containerized MBR Technology in Industrial Wastewater Treatment
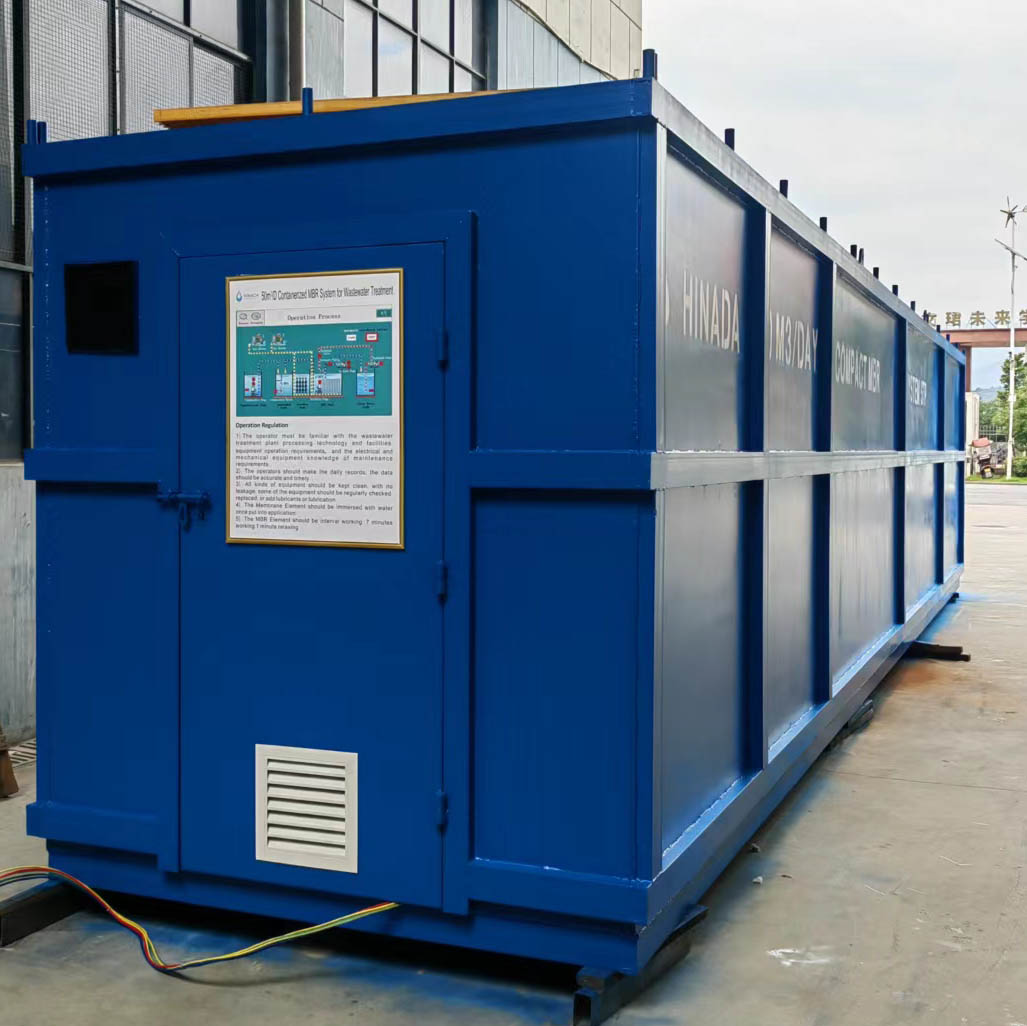
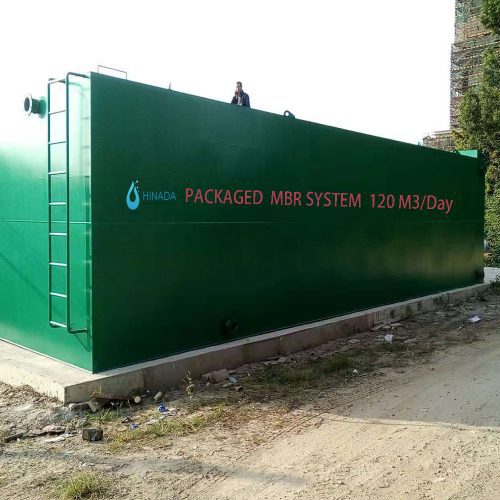
Containerized MBR systems represent the integration of advanced membrane filtration and biological treatment processes within a compact, mobile container. HINADA’s expertise as a leading Chinese manufacturer ensures that the containerized MBR system is engineered for rapid deployment, minimal footprint, and superior treatment performance.
undefined
MBR membrane module: The heart of the process, combining physical filtration and biological breakdown.
Containerized MBR system: Fully pre-fabricated, factory-tested, and ready for plug-and-play use.
Compact MBR plant: Fits limited spaces, perfect for industrial sites, construction camps, and remote locations.
The modular wastewater treatment approach allows for scalability and easy integration with existing infrastructure. From the procurement perspective, this modularity means reduced installation time and immediate return on investment.
Key Advantages of HINADA's Containerized MBR for Industrial Wastewater
1. Enhanced Filtration Efficiency with MBR Membranes
HINADA’s MBR membrane module technology ensures exceptional removal of suspended solids, bacteria, and viruses, delivering a consistent effluent quality suitable for reuse or safe discharge. The fine pore size of the membranes – typically 0.1 to 0.4 microns – guarantees high filtration efficiency, outperforming traditional activated sludge systems.
2. Plug and Play MBR: Fast Deployment and Commissioning
With the plug and play MBR design, industries benefit from minimal site preparation, rapid installation, and reduced commissioning times. This is crucial for buyers with tight project deadlines or temporary sites in need of mobile wastewater treatment solutions.
3. Energy-Saving and Operational Cost Reduction
HINADA’s energy-saving MBR systems utilize optimized aeration, low-energy membrane modules, and smart automation. This translates to significant operational cost savings – a key purchasing consideration that directly affects your bottom line.
4. Flexibility and Customization
With HINADA’s customized wastewater solution capability, each containerized MBR can be tailored to specific flow rates, pollutant loads, and site conditions. From industrial sewage treatment to high-strength MBR system for textile wastewater, our R&D engineers collaborate with buyers to design fit-for-purpose systems that align with your operational goals.
5. Compliance with Stringent Discharge Standards
Meeting local and international environmental regulations is non-negotiable for modern industries. HINADA’s container MBR unit consistently achieves effluent qualities that exceed discharge or reuse requirements, simplifying compliance and enhancing your corporate sustainability profile.
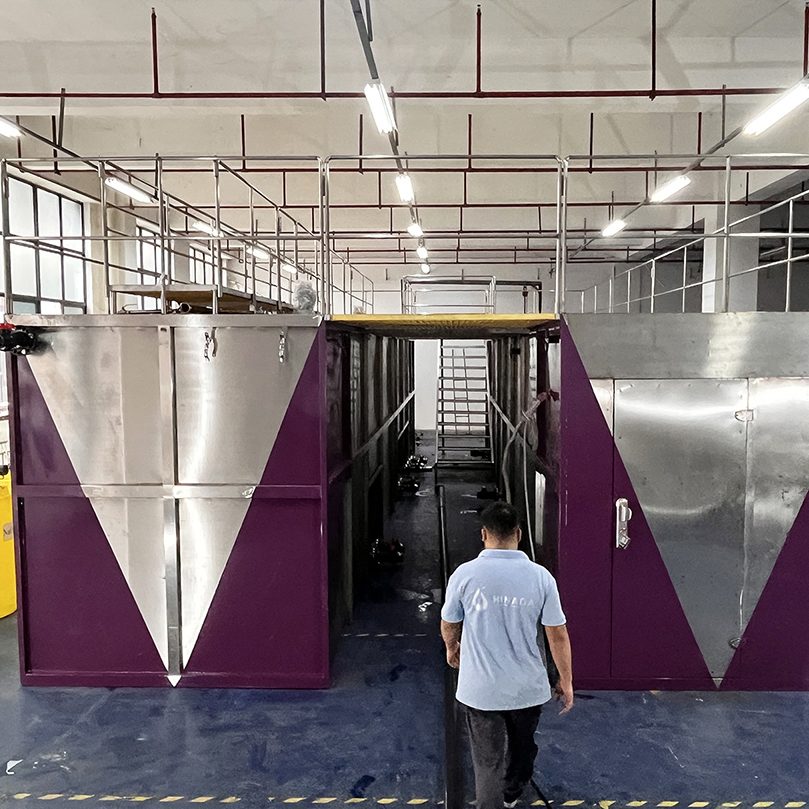
All-in-One Package: Each containerized MBR system integrates pretreatment, biological reactor, membrane module, controls, and a sludge handling compartment.
Advanced Controls: Automated PLC-based systems enable remote monitoring and operation, reducing O&M labor costs.
Scalable and Modular: Multiple compact MBR plants can be interconnected to handle increasing flows as your facility expands.
Easy Relocation: The mobile nature of containerized MBR for industrial wastewater ensures adaptability for changing operational needs or temporary sites.
For buyers, these technical features mean less risk, predictable performance, and minimized project management complexity – all critical factors in industrial procurement decisions.
Application Scenarios: Where HINADA Containerized MBR Excels
Textile and Dyeing Industry: Addressing high color, COD, and BOD loads with our MBR system for textile wastewater solutions.
Food & Beverage Processing: Ensuring safe discharge and potential water recycling.
Chemical and Petrochemical: Reliable treatment of complex, fluctuating wastewater streams.
Construction and Mining Camps: Mobile wastewater treatment for temporary or remote locations.
Municipal and Decentralized Installations: As a modular wastewater treatment option for expanding or upgrading existing capacity.
Each application leverages the adaptability and high-efficiency filtration that HINADA’s containerized MBR plant brings to the table, allowing buyers to secure a future-proof investment.
Integration Options: Containerized Reverse Osmosis System and Advanced Tertiary Treatment
For industries seeking ultra-pure water or zero-liquid discharge, HINADA offers seamless integration of containerized reverse osmosis system units following the MBR process. This multi-barrier approach guarantees removal of dissolved salts, heavy metals, and residual contaminants, meeting even the toughest reuse or disposal requirements.
Customer-Centric Customization: The HINADA Value Proposition
At HINADA, we understand that every buyer’s requirements are unique. Our consultation process involves in-depth analysis of your wastewater characteristics, space limitations, and regulatory targets. Whether you need a 10 m3/d customized wastewater solution or a 500 m3/d containerized MBR plant, our engineering team provides tailored designs, pilot testing, and ongoing technical support.
OEM & ODM service for partners seeking branded solutions.
Flexible procurement models, from single units to turnkey projects.
Pre-dispatch factory testing to ensure plug-and-play reliability.
Comprehensive after-sales service to maximize your investment value.
Procurement Insights: Why Choose HINADA as Your Supplier?
Professional buyers prioritize not only technical performance but also supply chain reliability, after-sales support, and total lifecycle cost. HINADA’s credentials as a seasoned Chinese manufacturer mean:
Competitive pricing due to high-volume production and efficient supply chain management.
Global project references to demonstrate proven performance.
Direct factory communication and transparent project management.
Timely delivery – our containerized systems are pre-fabricated for rapid shipment.
Our team of technical and commercial professionals is committed to ensuring a smooth procurement process from initial inquiry to site commissioning and beyond.
Case Study: MBR System for Textile Wastewater in Action
One of HINADA’s recent projects involved a leading textile manufacturer facing regulatory pressure to reduce discharge color and COD. By deploying a containerized MBR system followed by a containerized reverse osmosis system, the plant achieved a 95% reduction in color and met strict effluent standards, all within a compact site footprint. This success was enabled by our rapid design customization, pre-assembled delivery, and on-site technical training – factors that drive confident purchasing decisions.
Ongoing Support: Investing in Long-Term Partnership
Choosing HINADA means more than just purchasing equipment. We offer a full lifecycle partnership, including operator training, membrane replacement service, and process optimization. Buyers can rely on our experienced team to keep your containerized MBR for industrial wastewater running at peak efficiency, ensuring regulatory compliance and operational peace of mind.
Future Trends: Smart, Sustainable, and Automated Wastewater Solutions
As Industry 4.0 and environmental stewardship become central to industrial operations, HINADA is investing in smart controls, remote monitoring, and advanced analytics for containerized MBR plant solutions. This commitment to innovation guarantees that your procurement is not only for today’s needs but is also ready for tomorrow’s regulations and business models.
Conclusion: Secure Your Competitive Edge with HINADA Containerized MBR
For professional buyers seeking a reliable, efficient, and future-proof solution to industrial wastewater challenges, HINADA’s containerized MBR systems offer unmatched value. From filtration efficiency to cost savings, compliance, and operational flexibility, our technology is engineered to exceed your expectations and deliver measurable business benefits.
Contact HINADA Water Treatment Tech Co., Ltd. today to discuss your specific requirements and discover how our containerized MBR for industrial wastewater can improve your process efficiency and sustainability objectives.
Explore More: Related Solutions and Keywords
Containerized MBR for industrial wastewater
Containerized MBR system
Industrial sewage treatment
MBR membrane module
Compact MBR plant
Modular wastewater treatment
Container MBR unit
Customized wastewater solution
Plug and play MBR
Mobile wastewater treatment
Energy-saving MBR
MBR system for textile wastewater
Containerized reverse osmosis system
HINADA Chinese manufacturer
OEM/ODM containerized MBR
Ready to Upgrade Your Industrial Wastewater Treatment? Contact HINADA Now.