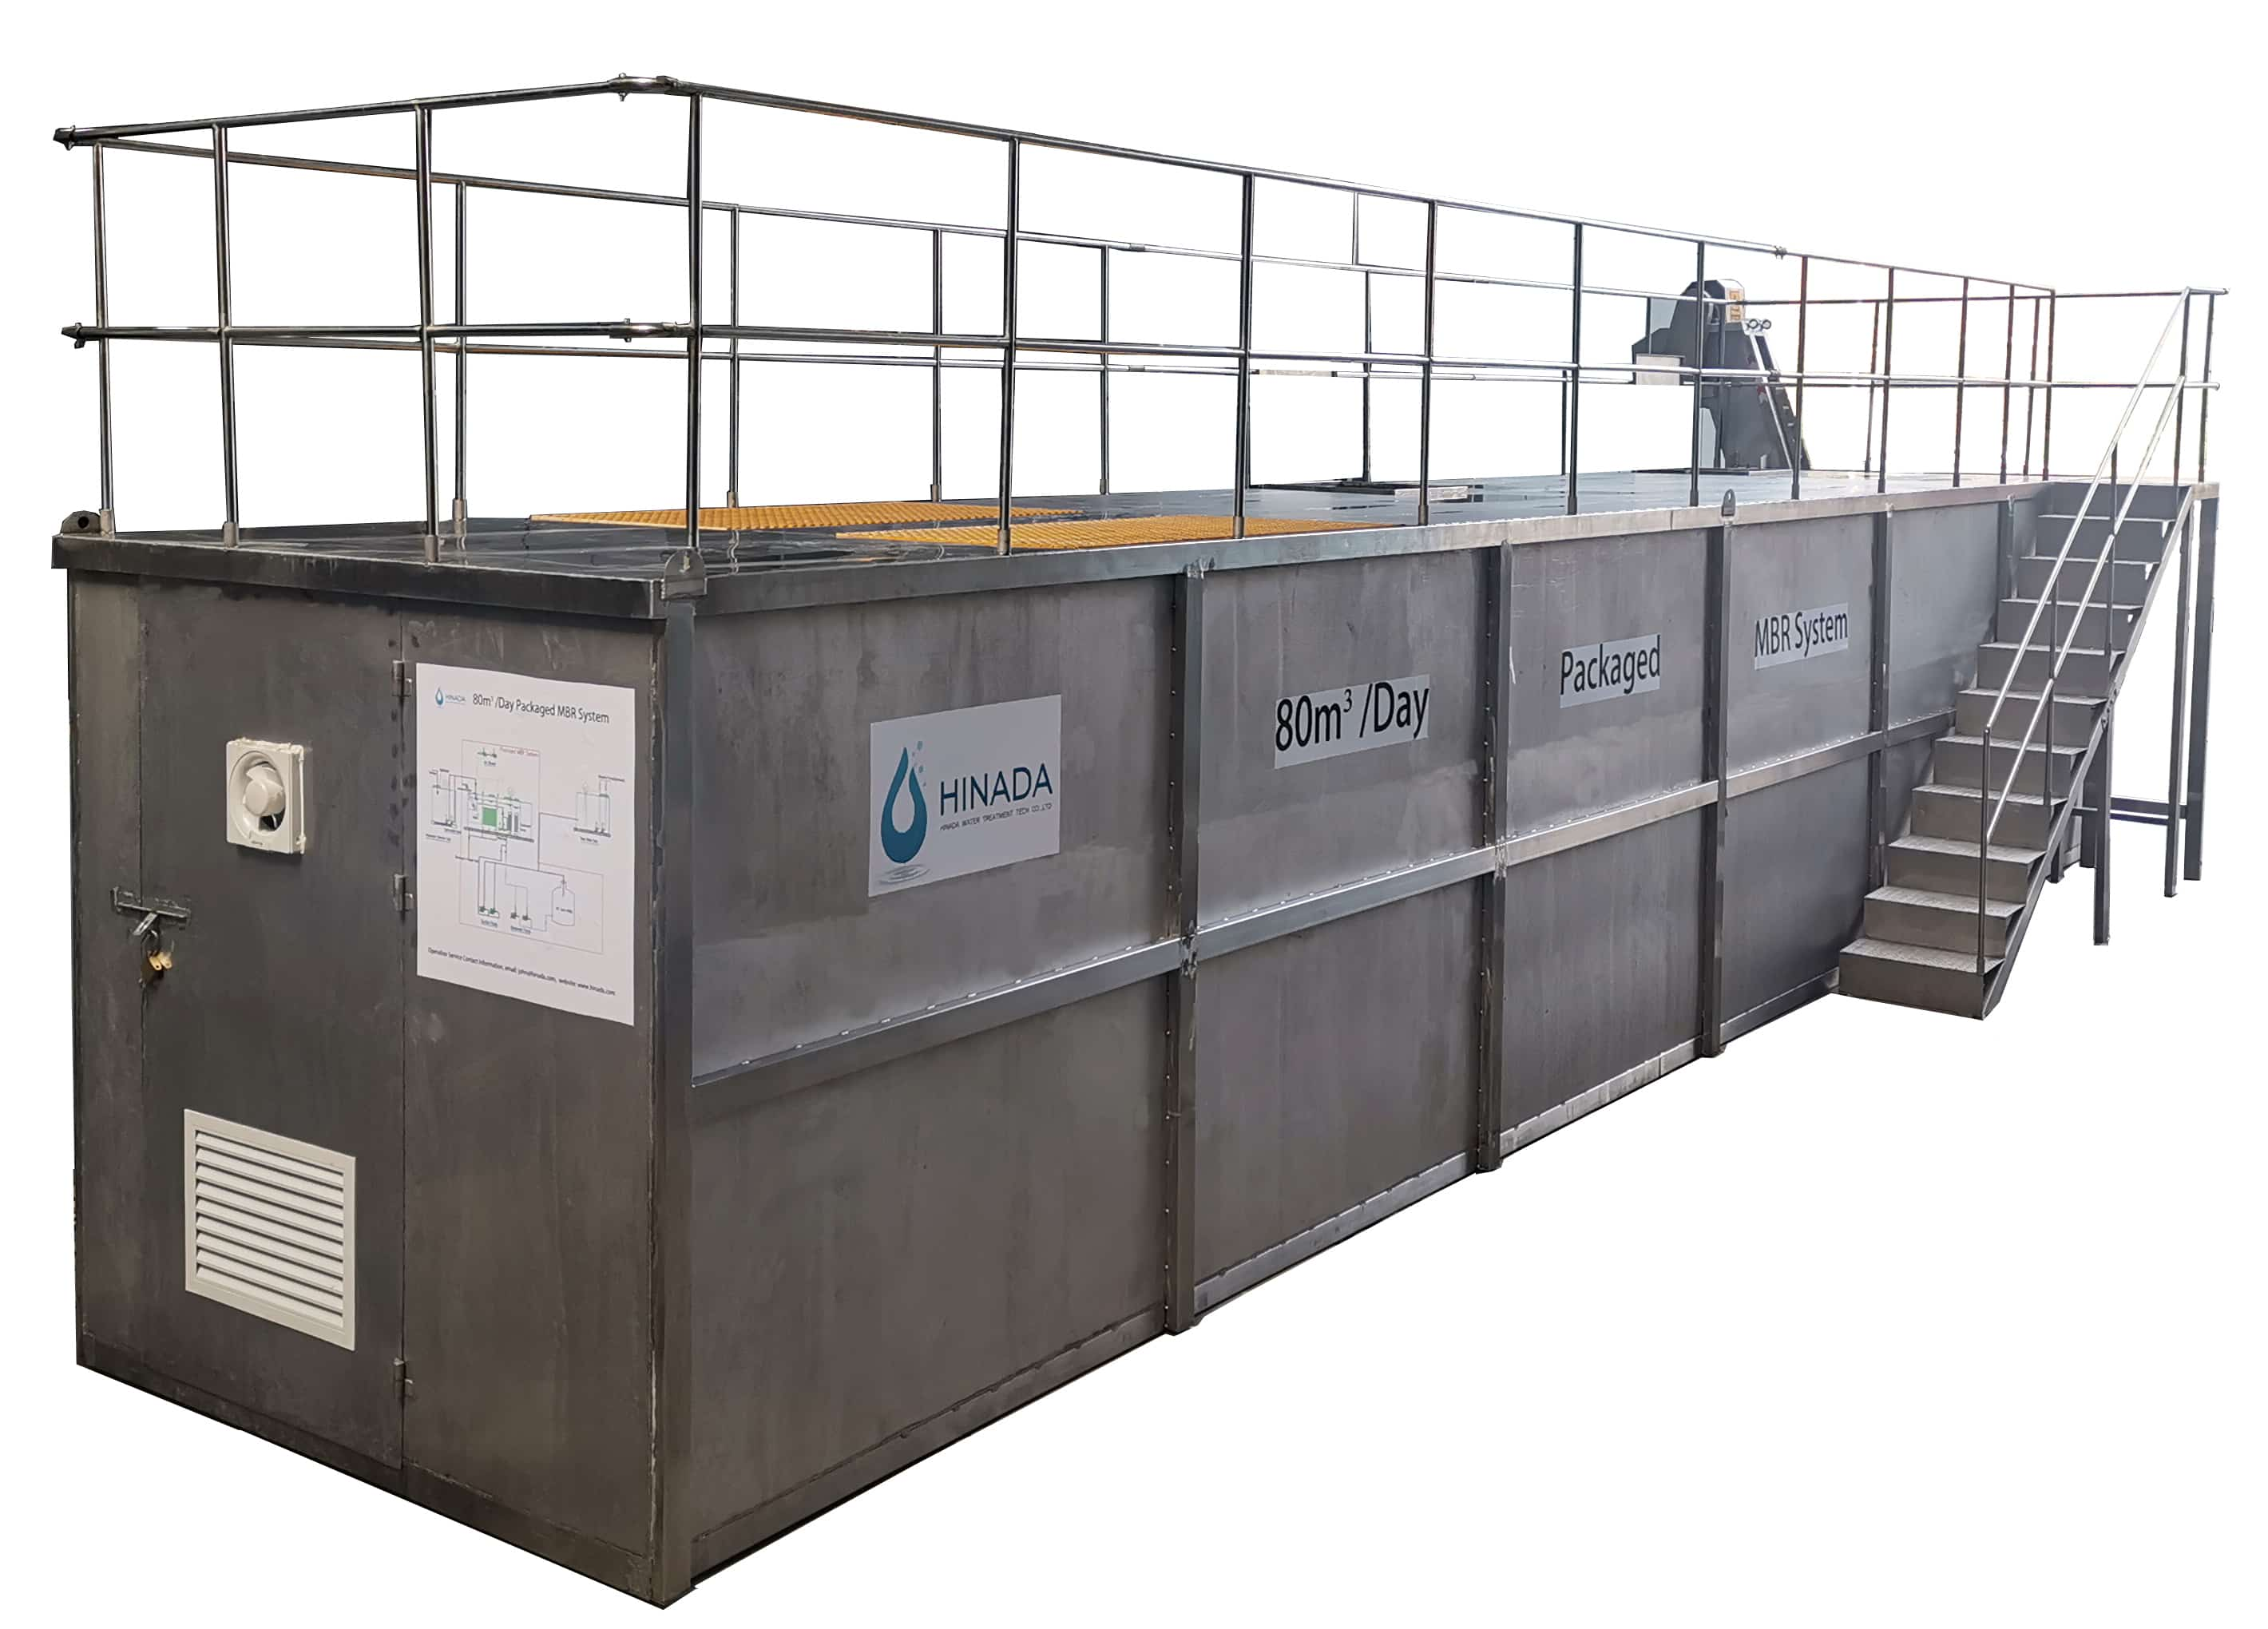
80 m³/day Containerized MBR System Delivered to Pakistan
80 m³/day Containerized MBR System Delivered to Pakistan
November 12, 2026
Author
Solution Provider, through a professional technical team, we provide customers with targeted equipment selection recommendations and comprehensive after-sales services, winning the trust and recognition of customers.
Sarah M.
80 m³/day Containerized MBR System Delivered to Pakistan
Hinada delivers an 80 m³/day containerized MBR wastewater treatment system to Pakistan, featuring PVDF membranes, compact design, and easy installation.
Hinada has completed the delivery of an 80 m³/day containerized MBR wastewater treatment system to a client in Pakistan. Designed for decentralized sewage treatment, this packaged MBR plant provides a compact and practical solution for projects with limited land, tight construction schedules, or challenging site conditions.
For clients who need a wastewater treatment plant without extensive on-site civil construction, a containerized MBR system offers a convenient alternative to traditional concrete treatment facilities.
Compact Wastewater Treatment in a Containerized Design
The 80 m³/day MBR system integrates key treatment processes into a standard container structure, including equalization, biological treatment, membrane separation, and disinfection.
At the heart of the system are Hinada's PVDF hollow-fiber MBR membrane modules. These membranes separate treated water from activated sludge, retaining suspended solids and biomass within the biological treatment process while producing clear treated effluent.
By integrating the main treatment equipment into one container, the system can be manufactured and pre-assembled at the factory before delivery. This reduces on-site installation work, minimizes the need for extensive civil construction, and helps simplify project implementation.
Easier Transportation, Installation, and Operation
For overseas wastewater treatment projects, transportation, installation, and local construction conditions can all affect project schedules and costs.
The containerized design helps address these challenges:
Factory pre-assembly: Main equipment and treatment components are integrated before shipment, reducing on-site assembly work.
Space-saving design: The compact structure is suitable for locations with limited available land.
Faster installation: Less civil construction and simpler site connections help shorten installation time.
Convenient operation: Integrated equipment and control systems support easier daily operation and monitoring.
Flexible applications: Suitable for decentralized sewage treatment at communities, commercial facilities, and remote sites.
The system is designed to simplify wastewater treatment plant installation while maintaining the advantages of MBR technology, including efficient solid-liquid separation and a compact treatment footprint.
80 m³/day Containerized MBR System: Delivery and Operation Video
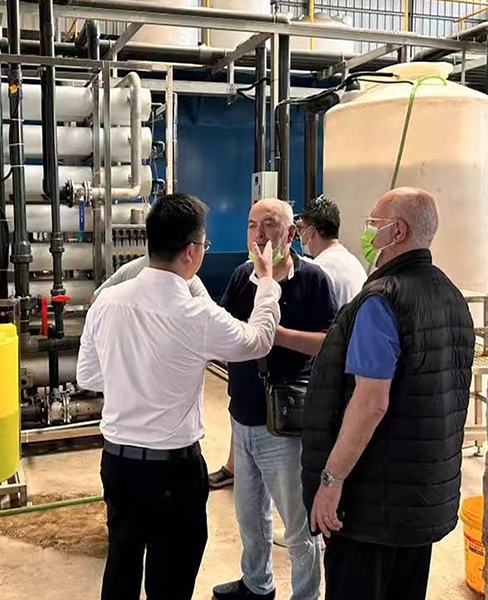
The project video shows the containerized MBR system during preparation, equipment integration, and operation.
Viewers can see the PVDF MBR membrane modules, blower and control equipment, as well as the overall containerized arrangement. It provides a practical reference for customers evaluating packaged MBR wastewater treatment plants for overseas projects.
Looking for a Containerized Wastewater Treatment Solution?
An 80 m³/day containerized MBR plant can be considered for community sewage treatment, commercial facilities, and other decentralized wastewater treatment applications.
Hinada provides packaged MBR systems and customized wastewater treatment solutions based on project capacity, wastewater characteristics, required effluent quality, and available installation space.
If you are planning a wastewater treatment project and considering a containerized MBR system, contact Hinada to discuss your treatment requirements and find a suitable solution.