Can MBR Membrane Bioreactor OEM Systems Enhance Water Purification
Can MBR Membrane Bioreactor OEM Systems Enhance Water Purification
October 13, 2026
Author
Solution Provider, through a professional technical team, we provide customers with targeted equipment selection recommendations and comprehensive after-sales services, winning the trust and recognition of customers.
Sarah M.
HINADA Water Treatment Tech Co., Ltd. (HINADA) delivers advanced MBR membrane bioreactor OEM systems that revolutionize water purification for municipal, industrial, and commercial buyers. By integrating cutting-edge MBR membrane technology with robust system engineering, HINADA's solutions offer superior effluent quality, reduced operational costs, low maintenance, and flexible OEM customization. Buyers benefit from space-saving modular designs, energy-efficient operations, and compliance with international standards—key factors influencing purchasing decisions. HINADA’s proven track record, comprehensive after-sales support, and dedication to sustainable water management make it a preferred partner globally. With a focus on solving real procurement challenges, HINADA’s MBR membrane bioreactor and MBR reactor products ensure buyers achieve environmental compliance, operational reliability, and the best value for investment. For those seeking to enhance water purification efficiency, HINADA stands as a trusted Chinese manufacturer and supplier of membrane bioreactor systems tailored to demanding project needs.
Introduction: The Demand for Advanced Water Purification Solutions
The rapid industrialization and urbanization across the globe have placed immense pressure on water resources, necessitating innovative water purification technologies. Hinada Water Treatment Tech Co., Ltd. (HINADA), a prominent Chinese manufacturer, has responded to this demand with its advanced MBR membrane bioreactor OEM systems. These systems, including mbr reactors, are at the forefront of wastewater treatment, offering superior efficiency, compact design, and environmental sustainability. This article delves deeply into how HINADA's membrane bioreactor solutions can address buyers' critical needs, integrating essential product keywords to ensure clarity, relevancy, and discoverability for procurement professionals seeking value-driven investments.
For decision-makers and technical procurement professionals, the selection of a reliable water purification system is not merely about equipment acquisition, but also about long-term operational efficiency and cost savings. HINADA’s MBR membrane bioreactor OEM systems stand out for several reasons:
Cutting-edge MBR membrane technology
Robust OEM system integration
Customizable capacities and modular designs
Efficient sludge reduction and superior effluent quality
Low operational and maintenance costs
When buyers prioritize reducing operational risk, minimizing downtime, and safeguarding compliance, HINADA’s dedication to quality and innovation is evident in every MBR reactor, MBR filtration system, and membrane bioreactor plant it manufactures.
Understanding the Core Technology: MBR Membrane Bioreactor & MBR Reactor
MBR Membrane Bioreactor Principle
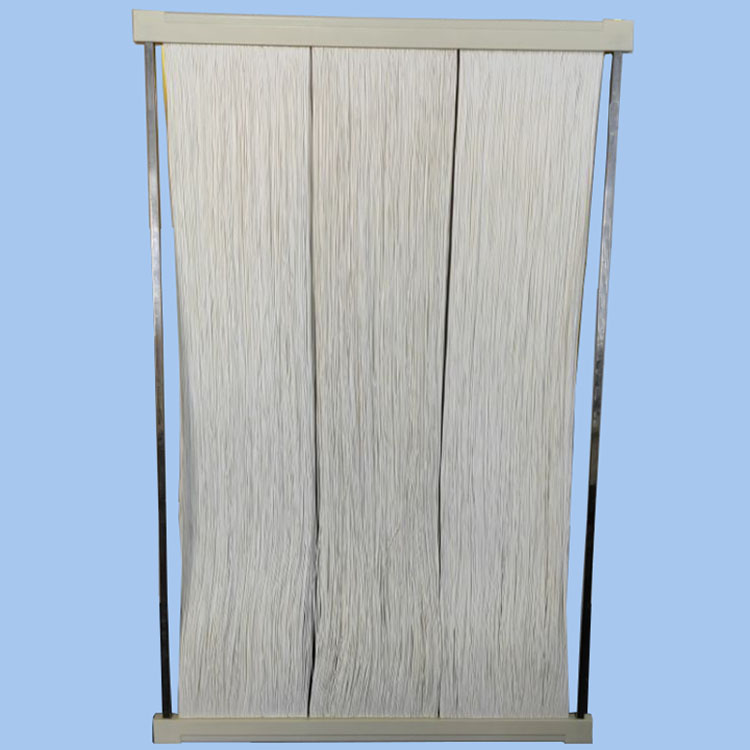
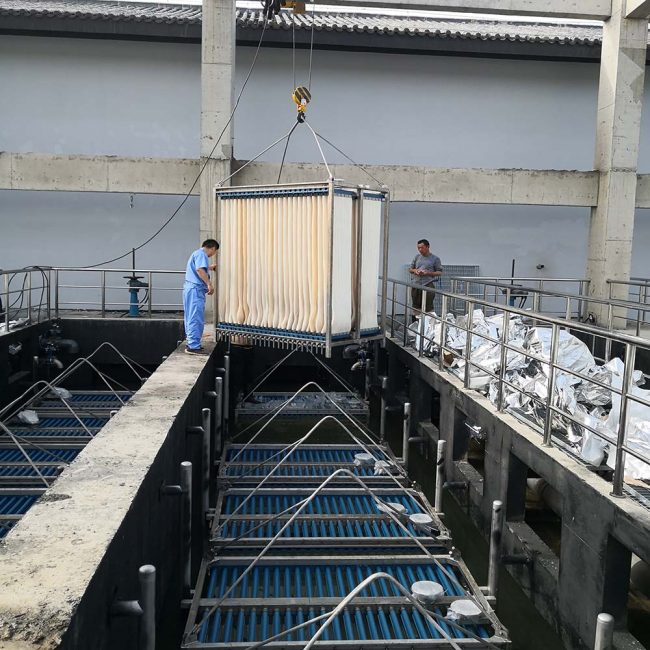
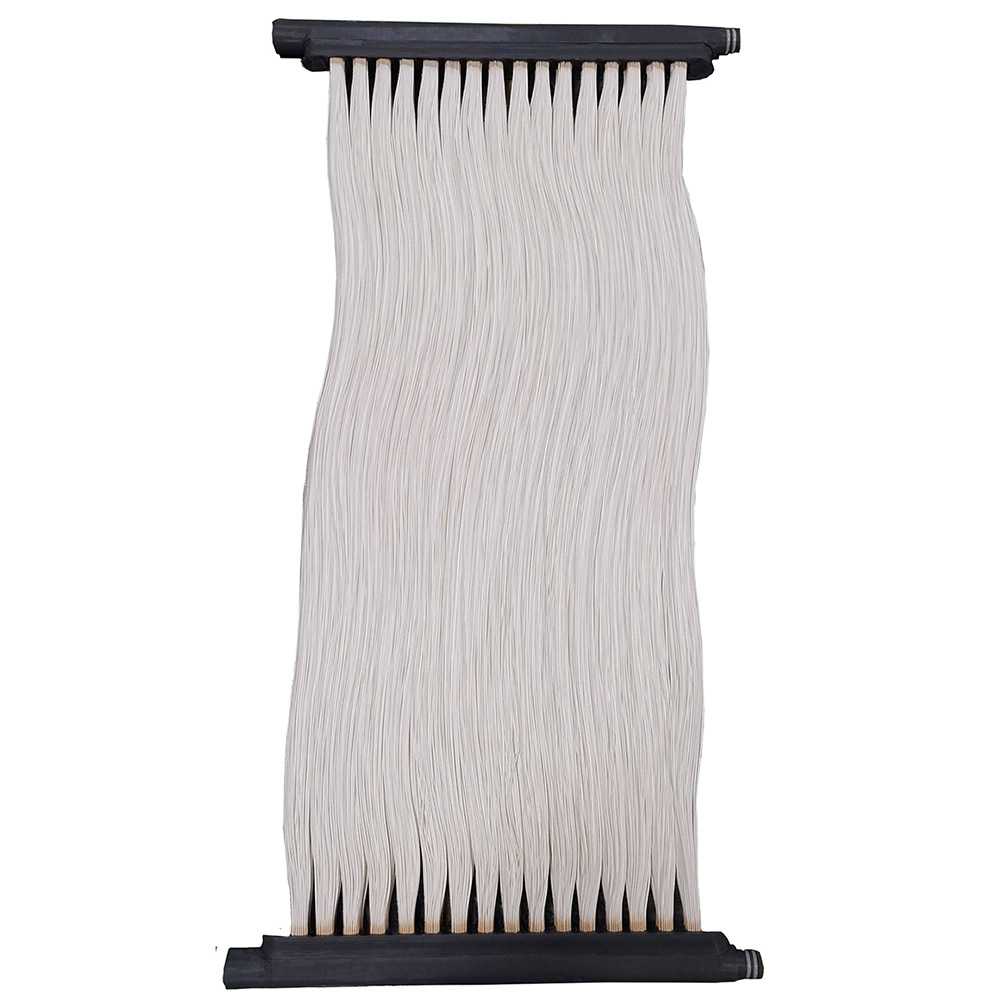
The mbr membrane bioreactor combines traditional biological treatment with advanced membrane filtration. HINADA utilizes submerged membrane modules within bioreactor tanks, effectively separating solids and liquids while retaining high concentrations of biomass. This configuration delivers consistent, high-quality effluent, surpassing conventional sewage treatment alternatives. As an MBR reactor functions, it ensures pathogens, organics, and suspended solids are efficiently removed, meeting stringent discharge and reuse standards.
Advantages of HINADA’s MBR System Solutions
1. Superior Effluent Quality
Buyers seeking membrane bioreactor wastewater treatment solutions often prioritize effluent quality. HINADA’s MBR membrane bioreactor OEM systems produce water suitable for industrial reuse, irrigation, or discharge into sensitive environments. The advanced mbr reactor and ultrafiltration features guarantee the reliable removal of bacteria and viruses, ensuring compliance with global regulatory standards.
2. Compact Footprint for Space Optimization
One of the key considerations for procurement managers is the physical footprint of water purification equipment. HINADA’s compact membrane bioreactor OEM systems allow for installation in space-constrained facilities, delivering high throughput from a minimal footprint. This is especially beneficial in urban and industrial zones where land costs are high.
3. Operational Cost Efficiency
Ensuring predictable and manageable operational costs is paramount for any buyer. HINADA’s MBR membrane bioreactor systems are designed for energy efficiency, automatic operation, and minimal chemical usage. The reduced sludge production means lower handling and disposal costs, aligning with purchasers’ interests in total cost of ownership.
4. Flexible OEM Customization
Every client’s water treatment needs are unique. HINADA excels in delivering flexible OEM membrane bioreactor systems that can be tailored to specific flow rates, influent compositions, and site requirements. Buyers benefit from modular MBR reactors, custom membrane choices, and integration with existing treatment processes.
Key Product Keywords Integrated in HINADA’s Portfolio
MBR membrane bioreactor
MBR reactor
Membrane bioreactor system
MBR filtration
MBR wastewater treatment
MBR membrane module
OEM membrane bioreactor
Compact MBR system
Industrial MBR plant
Ultrafiltration MBR system
Submerged MBR membrane
Biological wastewater treatment
Automatic MBR system
MBR effluent reuse
Energy-efficient MBR
Sludge reduction MBR
Containerized MBR plant
Custom MBR OEM
MBR plant installation
MBR module supplier
These product keywords highlight HINADA’s technical capabilities and broad product range, ensuring that procurement searches and technical evaluations match the right solution to your application.
Procurement Insights: What Buyers Value Most
1. Proven Performance and Track Record
As experienced procurement professionals know, successful purchasing relies on proven technology with verified references. HINADA’s MBR membrane bioreactor OEM systems have been deployed in numerous projects worldwide, from municipal water recycling to industrial wastewater treatment plants. Technical references and case studies are available to support due diligence and risk assessment processes.
2. Reliable After-Sales Service and Support
Post-installation support is a major concern for buyers. HINADA provides comprehensive technical support, from MBR plant commissioning to operator training and ongoing maintenance. This ensures minimized downtime, optimal system performance, and rapid response to any issues.
3. Compliance With International Standards
HINADA’s systems comply with global certifications, including ISO 9001:2015 for quality management and CE certification for safety. This gives procurement teams confidence in regulatory compliance and smooth project approval.
Technical Features of HINADA’s MBR Membrane Bioreactor OEM Systems
Feature
Benefit for Buyers
High-Flux PVDF/PS Membrane
Longer service life and stable performance
Integrated Modular Design
Easy expansion, transport, and installation
Automated Control Systems
Reduced labor costs, user-friendly interface
Low Sludge Generation
Reduced disposal costs and environmental impact
Chemical/Physical Cleaning Options
Extended membrane lifespan, reduced OPEX
Energy-Efficient Aeration
Lower electricity consumption
Wide Capacity Range (1-5000 m3/d+)
Suitable for small to large-scale projects
Customization: The OEM Advantage from HINADA
As a leading Chinese MBR membrane bioreactor OEM manufacturer, HINADA offers complete customization services:
Selection of membrane material and pore size
Design of modular MBR reactors for phased expansion
Integration with SCADA and PLC systems for automation
Customization of containerized, skid-mounted, or stationary plants
Adaptation for various influent types: municipal, industrial, or leachate
OEM buyers benefit from these flexibilities, ensuring an optimized fit for local feedwater quality, regulatory requirements, and footprint constraints.
Case Studies: Real-World Success with HINADA’s MBR Solutions
An electronics plant in East Asia sought a solution for high-COD, variable-load wastewater. HINADA deployed a compact MBR membrane bioreactor OEM system, achieving over 95% COD removal and enabling water reuse within the facility, reducing both costs and regulatory risks.
Municipal Sewage Upgrading – Urban Water Recycling
In a major city, a municipal authority required a robust, low-maintenance solution to upgrade an aging conventional sewage plant. HINADA’s modular MBR reactors were retrofitted, tripling effluent quality and increasing plant capacity without the need for additional land acquisition.
Frequently Asked Questions from Buyers
What is the typical lead time for HINADA’s MBR systems? Standard systems ship in 4-8 weeks; custom OEM builds depend on complexity.
Can MBR membrane bioreactors handle fluctuating influent conditions? Yes, HINADA’s advanced control systems ensure stable output even with variable loads.
Are spare parts and membranes readily available? HINADA maintains an international supply chain for fast part replacement and technical support.
Does HINADA provide training for operators? Yes, comprehensive training and remote support are standard in all OEM packages.
Can HINADA’s MBR reactors be integrated with existing treatment plants? Absolutely—modular and retrofit solutions are available to maximize existing infrastructure value.
Environmental and Economic Benefits
Reduce environmental footprint through minimized sludge and pollutant discharge
Achieve water reuse targets and reduce freshwater consumption
Lower total cost of ownership through energy savings and long membrane life
How to Procure: Steps Toward Seamless Project Execution
For global buyers and procurement teams interested in HINADA’s MBR membrane bioreactor OEM systems, the acquisition process is streamlined for efficiency:
Initial consultation and needs assessment
Technical solution proposal and system sizing
Quotation and commercial negotiation
OEM design and manufacturing
Quality inspection and FAT (Factory Acceptance Test)
Shipment, installation, and commissioning
After-sales service and long-term technical support
Why HINADA is the Preferred Partner for MBR Membrane Bioreactor OEM Solutions
HINADA’s reputation as a trusted MBR reactor and membrane bioreactor system supplier is built on:
Extensive technical expertise and R&D investment
Reliable OEM customization to meet diverse project needs
Transparent communication and global logistics capabilities
Commitment to sustainable, cost-effective water solutions
Conclusion: Invest in the Future of Water Purification with HINADA
Whether you are a municipal utility planner, an industrial facility manager, or a procurement officer seeking a competitive edge, HINADA’s MBR membrane bioreactor OEM systems are engineered for excellence. Innovative MBR reactors, flexible OEM services, and a proven global track record make HINADA your ideal partner for water purification projects—delivering reliable performance, environmental compliance, and real return on investment.
Contact HINADA Water Treatment Tech Co., Ltd. today to discuss your project, request a technical proposal, or arrange a factory visit. Discover how our MBR solutions can transform your water management strategy.