Solution Provider, through a professional technical team, we provide customers with targeted equipment selection recommendations and comprehensive after-sales services, winning the trust and recognition of customers.
Sarah M.
HINADA Water Treatment Tech Co., Ltd. is a leading Chinese manufacturer specializing in advanced membrane bioreactor (MBR) systems for water reuse. This detailed article explores why HINADA’s MBR solutions—including MBR wastewater treatment plants, MBR membrane modules, compact MBR systems, containerized MBR systems, MBR sewage treatment plants, submerged MBR systems, and more—are ideal investments for genuine buyers seeking sustainable, high-quality water treatment. Key advantages include superior effluent quality, modular scalability, low operational costs, regulatory compliance, and robust performance across industrial and municipal applications. HINADA integrates technical innovations such as biofilm reactors and UF membrane modules for enhanced treatment and ultra-fine filtration, meeting specialized buyer needs. The article adopts a professional perspective, addressing procurement priorities such as risk mitigation, lifecycle value, customization, and comprehensive technical support. With a procurement guide and a clear focus on buyer psychology, HINADA stands out as a trusted partner for efficient, sustainable, and scalable water reuse solutions. Genuine buyers are invited to contact HINADA for tailored engineering and world-class support.
Understanding Membrane Bioreactor (MBR) Systems for Water Reuse
As global water scarcity intensifies, industries, municipalities, and large-scale projects seek advanced solutions for reliable water reuse. At Hinada Water Treatment Tech Co., Ltd. (HINADA), we specialize in membrane bioreactor systems (MBR), offering state-of-the-art solutions for sustainable water treatment and reuse. This article explores the unique advantages that make HINADA MBR systems ideal for water reuse, focusing on key product features such as MBR system, MBR wastewater treatment plant, MBR membrane module, MBR membrane filtration, compact MBR system, containerized MBR system, MBR sewage treatment plant, submerged MBR system, industrial MBR system, municipal MBR system, and others crucial in buyer decision-making.
Why Choose HINADA MBR Systems for Water Reuse?
MBR System: Superior Water Quality and Efficiency
HINADA’s MBR systems utilize advanced membrane filtration technology to deliver consistently high-quality effluent suitable for non-potable reuse applications. Our MBR system integrates robust biological treatment with efficient membrane separation, ensuring removal of suspended solids, bacteria, and viruses. This translates to crystal-clear, odor-free recycled water—an essential requirement for industrial, municipal, and commercial buyers looking to minimize operational risks and maximize water reuse potential.
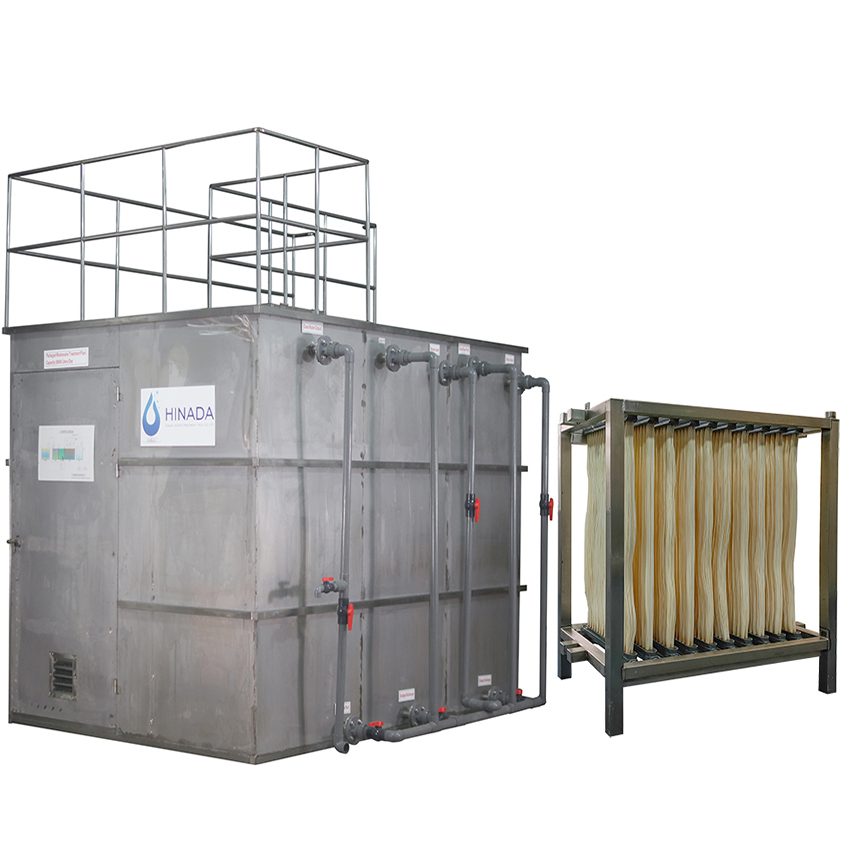
HINADA offers scalable MBR wastewater treatment plant designs tailored for industrial complexes, municipal infrastructure, and decentralized water reuse projects. Buyers benefit from modularity, rapid deployment, and low footprint, making our MBR plants ideal for retrofitting existing facilities or launching new sustainable initiatives. With proven track records in textile, pharmaceutical, food processing, and municipal sectors, HINADA ensures flexible capacity and customized engineering for optimal performance.
MBR Membrane Module: High-Performance Filtration at the Core
The heart of any MBR system is its MBR membrane module. HINADA employs proprietary ultrafiltration membranes with high flux, exceptional durability, and low fouling characteristics. These modules guarantee long service life and stable filtration performance, easing maintenance burdens and reducing operational costs for buyers. Our membrane modules are engineered for easy replacement and compatibility with a wide range of system configurations, an attractive feature for procurement professionals prioritizing lifecycle value.
MBR Membrane Filtration: Reliable Removal of Contaminants
MBR membrane filtration by HINADA ensures reliable removal of harmful contaminants, including pathogens, organic matter, and fine particulates. Whether for industrial reuse, irrigation, or cooling water applications, our membrane filtration process exceeds regulatory standards and delivers peace of mind to buyers. Advanced anti-fouling coatings and optimized module design minimize cleaning cycles, supporting cost-effective, continuous operation.
Compact MBR System: Space-Saving and High-Efficiency
For buyers with limited space or challenging site conditions, HINADA’s compact MBR system offers a powerful solution. Designed for both new installations and facility upgrades, our compact MBR systems feature integrated tanks, minimal piping, and plug-and-play automation. These systems are ideal for hotels, resorts, schools, and remote sites where space efficiency is paramount.
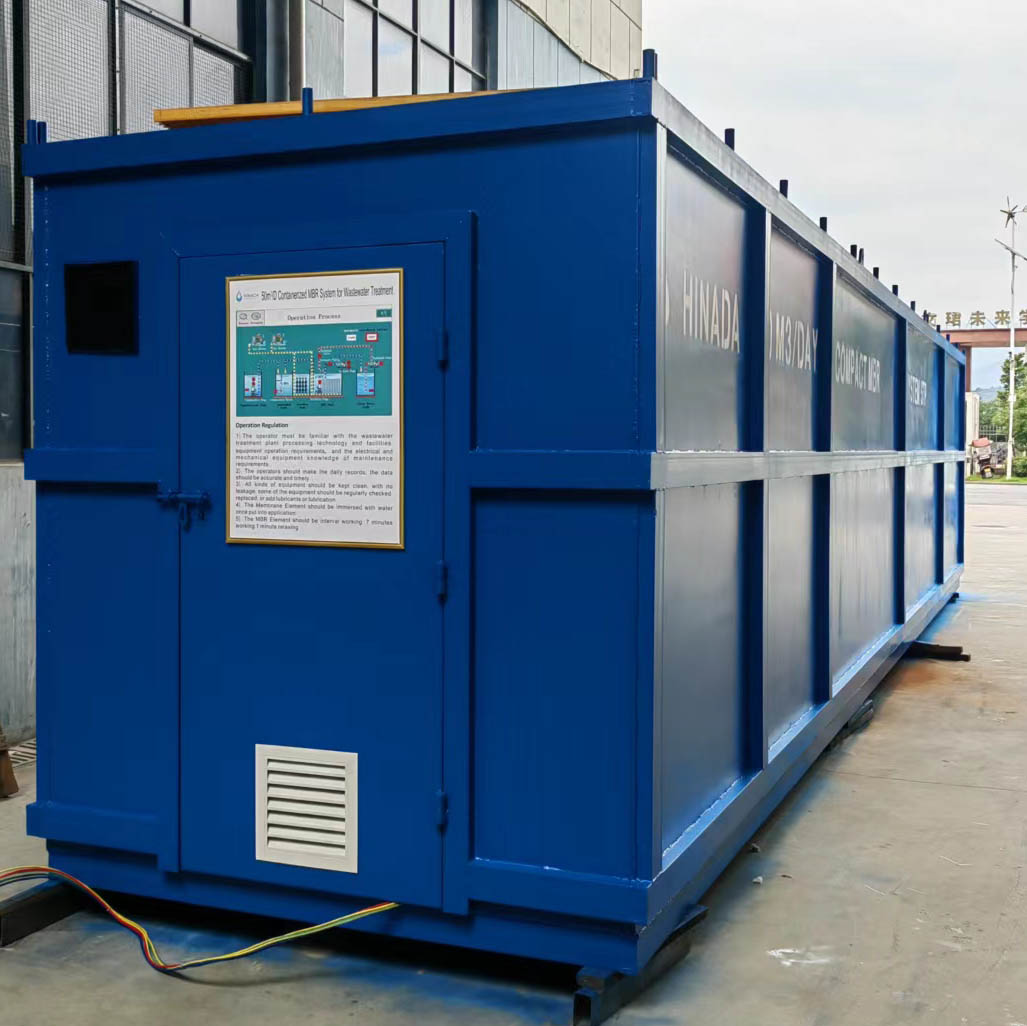
HINADA containerized MBR system brings the advantages of mobility, fast commissioning, and robust performance to water reuse projects. Delivered in ISO-standard containers, these turnkey units are favored by buyers in emergency response, construction, mining, and remote community applications. Our containerized MBR systems support rapid installation, scalability, and easy relocation—key buying factors for flexible project requirements.
MBR Sewage Treatment Plant: Sustainable Management of Municipal Wastewater
Municipal buyers seeking modern solutions for sewage management find HINADA’s MBR sewage treatment plant a reliable investment. Our plants ensure compliance with stringent discharge standards and facilitate water reuse for landscaping, agriculture, and industrial supply. With integrated automation and remote monitoring capabilities, municipalities gain operational transparency, efficiency, and long-term reliability.
Submerged MBR System: Advanced Process Control and Energy Efficiency
HINADA’s submerged MBR system is engineered for high throughput, energy efficiency, and stable operation. Submerged membrane modules reduce aeration costs and support lower energy consumption. Buyers benefit from advanced process control, automated membrane cleaning, and improved resilience to load fluctuations—factors that lower operating costs and enhance system longevity.
Industrial MBR System: Robust Performance for Challenging Wastewater
Industries facing complex wastewater streams rely on HINADA’s industrial MBR system for robust treatment. Our systems handle high organic loads, variable flow rates, and corrosive environments with ease. Buyers in manufacturing, chemical processing, and power generation value the reliability, regulatory compliance, and low maintenance requirements of HINADA’s MBR solutions.
Municipal MBR System: Meeting Urban Water Reuse Needs
Urban buyers need efficient and scalable water reuse solutions. HINADA’s municipal MBR system supports decentralized, community-scale projects, urban redevelopment, and expansion of existing treatment infrastructure. With compact footprints and modular scalability, our systems facilitate sustainable urban growth and resource conservation.
Additional Benefits for Discerning Buyers
Easy Integration: HINADA MBR systems are designed for seamless integration with existing water treatment facilities, providing buyers with upgrade flexibility.
Comprehensive Support: From initial consultation to aftersales service, HINADA provides expert technical guidance, training, and maintenance support.
Cost Efficiency: Low operating costs, minimized chemical usage, and reduced labor requirement make HINADA MBR systems attractive for long-term investment.
Regulatory Compliance: All systems meet or exceed local and international standards, ensuring hassle-free regulatory approval for buyers.
Integration of Biofilm Reactor and UF Membrane Module
Biofilm Reactor: Enhanced Biological Treatment
HINADA also offers solutions featuring a biofilm reactor, which supplements the traditional MBR system. By providing additional surface area for microbial growth, biofilm reactors boost organic degradation, optimize nutrient removal, and increase process stability—qualities valued by buyers seeking robust treatment performance under variable loads.
UF Membrane Module: Ultra-Fine Filtration for Higher Purity
Our UF membrane module delivers ultra-fine filtration, complementing the MBR membrane module for even higher water purity. For buyers in pharmaceutical, electronics, and food industries, UF membrane modules are critical for meeting strict quality requirements and regulatory standards.
Buyer Psychology: Why HINADA MBR Systems Stand Out
Risk Mitigation and Reliability
Professional buyers prioritize risk mitigation and operational reliability. HINADA’s track record, engineering expertise, and comprehensive quality control ensure each MBR system delivers consistent, dependable performance—minimizing downtime and operational surprises.
Lifecycle Value and ROI
Experienced procurement personnel seek solutions with optimal lifecycle value. Our MBR systems feature easy-to-maintain modules, low energy consumption, and long service life, supporting strong return on investment for buyers. Transparent cost projections, warranty, and aftersales support further enhance buyer confidence.
Customization and Technical Support
Buyers value customization and responsive technical support. HINADA offers tailored engineering, on-site commissioning, and remote monitoring, ensuring that each MBR solution aligns perfectly with project requirements and buyer expectations.
Key Product Keywords Integrated in HINADA Solutions
Product Keyword
Application/Benefit
MBR system
Core water reuse solution, high-quality effluent
MBR wastewater treatment plant
Scalable, industry-specific, modular
MBR membrane module
High durability, easy replacement
MBR membrane filtration
Reliable removal of pathogens/contaminants
Compact MBR system
Space-saving, integrated design
Containerized MBR system
Plug-and-play, mobile deployment
MBR sewage treatment plant
Municipal compliance, water reuse
Submerged MBR system
Energy efficiency, advanced automation
Industrial MBR system
Robust, high-load treatment
Municipal MBR system
Urban water reuse, decentralized
Biofilm reactor
Enhanced biological treatment
UF membrane module
Ultra-fine filtration, highest purity
Professional Perspective: HINADA as Your Trusted Manufacturer
HINADA Water Treatment Tech Co., Ltd. is a leading Chinese manufacturer in the global MBR market. Our team comprises experienced technical personnel and procurement specialists who understand the nuanced needs of buyers—delivering solutions for every scale, application, and regulatory environment. We offer quality certifications, rigorous factory testing, and transparent project communication, making us the preferred partner for discerning clients worldwide.
HINADA MBR System Procurement Guide
Step 1: Define project requirements and choose the right MBR system variant (compact, containerized, submerged, municipal, industrial).
Step 2: Evaluate site constraints, capacity needs, and integration options.
Step 3: Consult HINADA’s technical sales team for customized engineering and solution design.
Step 4: Review lifecycle cost analysis, warranty, and aftersales service plans.
Step 5: Confirm order and initiate production, factory acceptance testing, and shipment logistics.
Step 6: Receive on-site commissioning, training, and ongoing technical support from HINADA.
Conclusion: Invest in HINADA MBR Systems for Sustainable Water Reuse
Buyers looking for reliable, efficient, and scalable water reuse solutions will find that HINADA’s range of MBR systems—featuring advanced membrane technology, modular engineering, and comprehensive support—offer unmatched value. Whether your project calls for an MBR wastewater treatment plant, compact MBR system, containerized MBR system, or custom solution with integrated biofilm reactor and UF membrane module, HINADA delivers results with professionalism and technical excellence. Contact us today to discuss your water reuse project and discover the benefits of partnering with China’s premier MBR manufacturer.