Choosing a Wastewater Treatment System manufacturer for Tough Needs
Choosing a Wastewater Treatment System manufacturer for Tough Needs
September 30, 2026
Author
Solution Provider, through a professional technical team, we provide customers with targeted equipment selection recommendations and comprehensive after-sales services, winning the trust and recognition of customers.
Sarah M.
HINADA Water Treatment Tech Co., Ltd. is a globally recognized manufacturer of wastewater treatment equipment, hollow fiber ultrafiltration membranes, submerged MBR membrane modules, integrated packaged wastewater treatment systems, and DAF systems. Founded in 2012 in Guangzhou, China, HINADA expanded its manufacturing base to Chenzhou, Hunan Province, and now serves clients in over 75 countries across Asia, Africa, Europe, and the Americas. The company focuses on two core technology pillars: hollow fiber ultrafiltration and MBR membranes for precise physical separation, and intelligent integrated wastewater treatment equipment for municipal, industrial, and decentralized applications. Its product range includes PVDF and PVC hollow fiber UF membranes, submerged MBR membrane modules, containerized MBR systems, packaged wastewater treatment plants, DAF systems, ultrafiltration systems, and industrial reverse osmosis systems. With more than 13 years in the water treatment industry and 10 years of membrane and equipment manufacturing experience, HINADA provides a complete ecosystem from membrane R&D and component manufacturing to equipment fabrication and turnkey solution delivery. The company supports projects from design, supplying, installation support, and commissioning to training. Key application fields include industrial wastewater treatment and reuse, municipal sewage treatment and water recycling, rural decentralized water supply and sanitation, and drinking water purification from surface water and groundwater. HINADA also participates in international water treatment exhibitions, bringing Chinese membrane technology to regions where clean water is most needed. For tough wastewater needs, choosing a manufacturer with proven membranes, integrated equipment, global experience, and end-to-end support can reduce project risk and improve long-term reliability.
Choosing a Wastewater Treatment System Manufacturer for Tough Needs
When industrial, municipal, or decentralized projects face difficult wastewater conditions, the choice of manufacturer matters as much as the treatment process itself. A reliable partner must combine membrane science, equipment fabrication, and project support. HINADA Water Treatment Tech Co., Ltd., known as HINADA, has built its reputation on that combination since 2012.
Founded in Guangzhou, China, HINADA later expanded its manufacturing base to Chenzhou, Hunan Province. Today it serves clients in more than 75 countries across Asia, Africa, Europe, and the Americas. That global footprint reflects a practical focus: delivering systems that work in real-world conditions, not only in controlled pilot studies.
undefined
Why Tough Needs Demand More Than Standard Equipment
Tough needs can include high-strength industrial wastewater, variable municipal flows, remote rural sanitation, or surface water and groundwater purification. In these settings, suspended solids, bacteria, colloids, and macromolecular organics can quickly overwhelm conventional designs. HINADA addresses these challenges through two core technology pillars.
Hollow Fiber Ultrafiltration and MBR Membranes
The first pillar is hollow fiber ultrafiltration, including UF and MBR membranes. These membranes provide precise physical separation of suspended solids, bacteria, colloids, and macromolecular organics. HINADA manufactures PVDF and PVC hollow fiber UF membranes, along with submerged MBR membrane modules. For projects needing compact biological treatment and high-quality effluent, submerged MBR modules can be a strong fit.
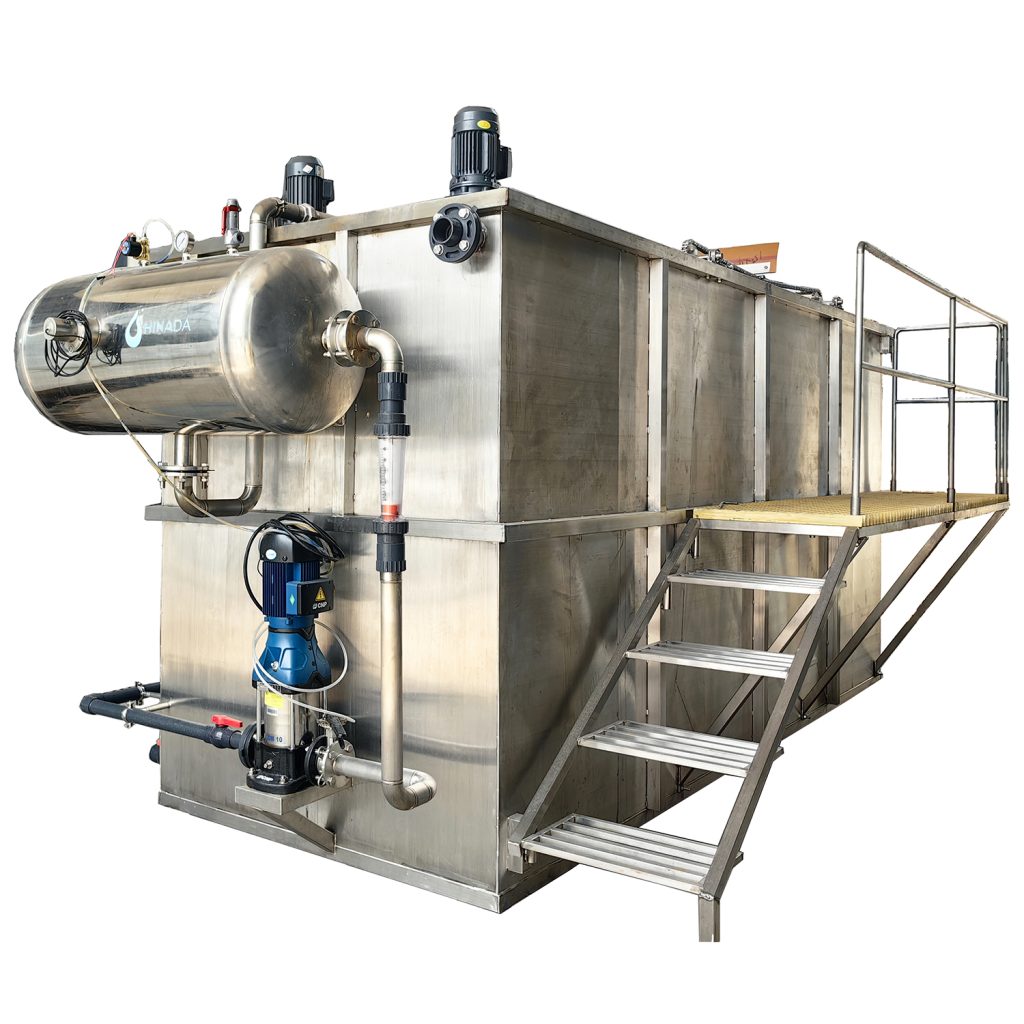
The second pillar is intelligent integrated wastewater treatment equipment. This includes containerized MBR systems, packaged wastewater treatment plants, dissolved air flotation (DAF) systems, ultrafiltration systems, and industrial reverse osmosis (RO) systems. These ready-to-install solutions serve municipal, industrial, and decentralized applications.
From Components to Turnkey Delivery
HINADA offers a complete ecosystem from membrane R&D and component manufacturing to equipment fabrication and turnkey solution delivery. With more than 13 years in the water treatment industry and 10 years of water treatment membrane and equipment manufacturing experience, the company provides an integrated solution from design, supplying, installation support, and commissioning to training.
Key Application Fields
Industrial wastewater treatment and reuse
Municipal sewage treatment and water recycling
Rural decentralized water supply and sanitation
Drinking water purification, including surface water and groundwater
What to Look for in a Manufacturer for Tough Needs
Buyers should examine membrane expertise, because it determines separation performance, fouling resistance, and lifespan. They should also review integrated equipment capability, which reduces interface risk between membranes, tanks, controls, and skids. Global project experience prepares a manufacturer for varied regulations, climates, and feed waters. Finally, support from design to training protects performance after commissioning.
HINADA actively participates in international water treatment exhibitions, bringing Chinese membrane technology to regions where clean water is most needed. For buyers facing tough needs, this kind of manufacturer can offer both proven products and practical delivery.
Conclusion
Choosing a wastewater treatment system manufacturer is a long-term decision. HINADA Water Treatment Tech Co., Ltd. combines hollow fiber UF and MBR membranes, integrated packaged systems, DAF, UF, and RO equipment with a global service mindset. For demanding projects, that blend of technology, manufacturing, and support is often the difference between a system that simply runs and one that performs reliably for years.