Containerized MBR System Manufacturer Offers Innovative Water Recycling Solutions
Containerized MBR System Manufacturer Offers Innovative Water Recycling Solutions
November 03, 2026
Author
Solution Provider, through a professional technical team, we provide customers with targeted equipment selection recommendations and comprehensive after-sales services, winning the trust and recognition of customers.
Sarah M.
Hinada Water Treatment Tech Co., Ltd. (HINADA) is a leading Chinese manufacturer specializing in innovative water recycling and purification solutions, with a particular focus on containerized MBR (Membrane Bioreactor) systems. HINADA’s extensive product range encompasses containerized MBR plants, modular and compact MBR systems, industrial MBR solutions, mobile water treatment units, and related technologies such as Dissolved Air Flotation (DAF) systems and UF membrane modules. These robust, plug-and-play systems offer buyers rapid deployment, scalability, high-quality effluent, and reliable operation in diverse environments. HINADA’s approach is grounded in understanding the unique needs of procurement professionals and technical decision-makers, offering tailored solutions, comprehensive after-sales support, and compliance with international standards (including ISO and CE certifications). The company’s commitment to sustainability, advanced automation, and technical excellence helps clients achieve regulatory compliance, reduce operational costs, and enhance water reuse. Real-world case studies demonstrate the effectiveness of HINADA’s solutions in industrial parks, emergency response, and municipal upgrades worldwide. For buyers seeking a trusted, innovative partner in water recycling, HINADA stands out as a top choice for durable, efficient, and future-ready wastewater treatment technologies.
Introduction to HINADA's Advanced Water Treatment Technologies
In today's rapidly developing world, water scarcity and water pollution are increasingly pressing issues that demand immediate and sustainable solutions. Hinada Water Treatment Tech Co., Ltd. (abbreviated as HINADA), a leading Chinese manufacturer, stands at the forefront of water purification and recycling innovations. HINADA is renowned for its containerized MBR system solutions, addressing the urgent needs of industries, municipalities, and commercial clients worldwide. Our advanced portfolio includes MBR wastewater treatment plant, membrane bioreactor system, containerized MBR plant, industrial MBR system, modular MBR wastewater system, compact MBR system, containerized membrane bioreactor, mobile mbr water treatment plant, MBR package plant, containerized sewage treatment plant, and portable MBR plant—offering a comprehensive spectrum of water recycling and treatment solutions.
Deep Dive: Why Choose HINADA’s Containerized MBR System?
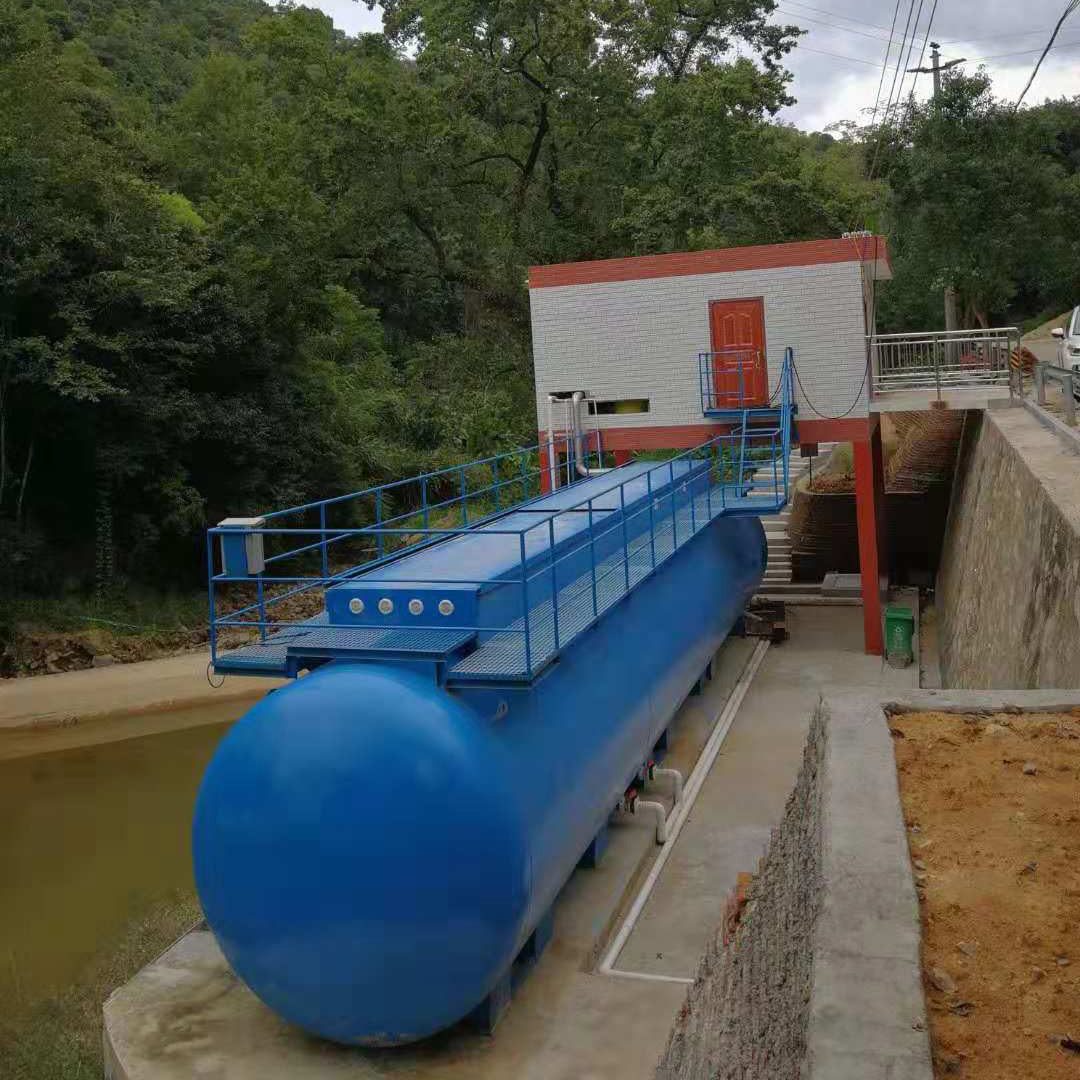
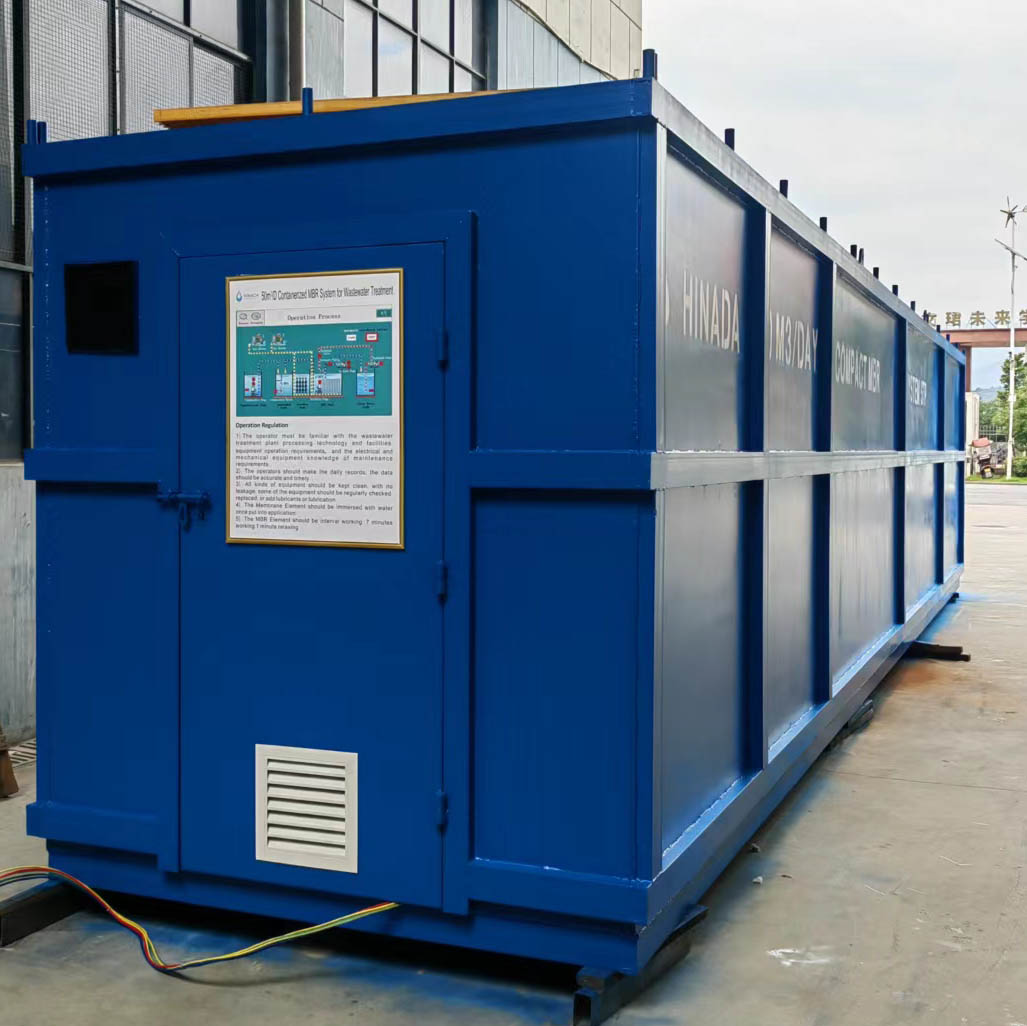
Procurement experts and technical professionals understand that selecting the right water treatment solution is about more than just price—it’s about reliability, scalability, and long-term performance. HINADA’s containerized MBR system sets a new benchmark in the water treatment industry by offering modular, plug-and-play solutions that integrate seamlessly into both new and existing infrastructures. Our containerized MBR plant boasts a robust design for harsh environments, minimizes space requirements, and ensures rapid deployment—critical factors for buyers seeking efficiency and flexibility.
Plug-and-play modular design: Saves on installation and commissioning time.
Scalable capacity: Expand treatment capacity quickly as demand grows.
High-quality effluent: Meets and surpasses international discharge standards.
Low footprint: Perfect for urban and industrial areas with limited space.
All-weather operation: Engineered for reliability in diverse climates.
Our MBR wastewater treatment plant is lauded for its highly efficient organic removal, nutrient elimination, and advanced filtration. Utilizing state-of-the-art membrane bioreactor system technology, HINADA’s systems guarantee crystal-clear effluent, ideal for water recycling and reuse in irrigation, industrial processes, or even potable applications after further treatment. As a key Containerized MBR System manufacturer, we prioritize both performance and cost-effectiveness, ensuring our clients achieve a rapid return on investment.
2. Containerized and Mobile MBR Solutions
Designed for mobility and rapid deployment, our containerized MBR plant and mobile MBR water treatment plant are perfect for emergency response, temporary project sites, remote locations, and expansion of existing treatment facilities. These solutions come pre-assembled and tested, drastically shortening the time from order to operation.
3. Modular and Compact MBR Systems
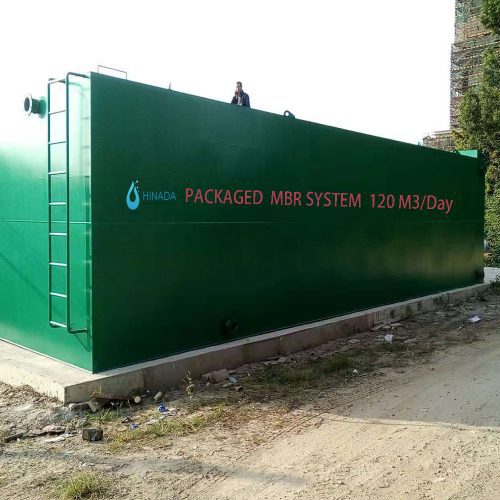
Our modular MBR wastewater system and compact MBR system provide buyers with unmatched flexibility. Whether for small communities, industrial estates, or decentralised applications, these systems are easily integrated, expanded, or relocated as needs evolve.
Technical Excellence: Key Features and Innovations
Advanced Membrane Technology: Our membrane bioreactor system uses high-performance, low-fouling membranes that extend operational cycles and reduce maintenance costs.
Intelligent Process Control: Automated monitoring and control ensure compliance and optimize operational efficiency, reducing the need for onsite staff.
Energy Efficiency: HINADA’s solutions are engineered for minimal energy consumption, reducing operational expenses for buyers.
Robust, Corrosion-Resistant Construction: Our containerized systems are built to last, using marine-grade materials for reliable performance in challenging environments.
Odor and Noise Control: Fully sealed and insulated containers minimize odor emissions and noise, ensuring community and workplace comfort.
Integration of Dissolved Air Flotation (DAF) System and UF Membrane Module
At HINADA, we understand the importance of pre-treatment and final polishing in advanced water recycling facilities. Our Dissolved Air Flotation (DAF) system can be integrated upstream of the MBR to efficiently remove suspended solids, oils, and greases, ensuring membrane longevity and stable operation. Downstream, the UF membrane module can be added for final water polishing, supporting ultrafiltration to achieve higher purity levels for reuse or discharge. These enhancements further empower our buyers to meet stringent regulatory requirements and maximize water recovery rates.
Buyer-Centric Approach: Understanding Needs and Delivering Value
1. Project Customization and Expert Consultation
Every project is unique, with specific regulatory, environmental, and budgetary requirements. HINADA’s technical consultants work closely with procurement professionals and engineers to define the best-fit solution, from portable MBR plant sizing to system automation, and from effluent standards to local installation requirements. Our deep experience as a Chinese manufacturer allows us to offer competitive pricing without compromising on quality or compliance.
2. Comprehensive After-Sales Service and Support
Our partnership doesn’t end at delivery. HINADA provides continuous technical assistance, spare parts supply, remote monitoring options, and on-site training to maximize system uptime and performance. We understand that buyers need reliability and responsive support to achieve operational goals.
HINADA’s Commitment to Sustainability and Innovation
Sustainability is at the heart of HINADA’s mission. Our containerized MBR system solutions help clients reduce water consumption, lower environmental impact, and achieve green certification for their operations. By advancing technology in the containerized sewage treatment plant and MBR package plant sectors, we empower industries and communities to thrive even as water resources become increasingly scarce.
International Standards and Certifications
HINADA’s manufacturing processes adhere to global standards, including ISO 9001, CE marking, and other region-specific certifications. This ensures seamless project approvals and peace of mind for international buyers. Our extensive portfolio and references including successful installations in Europe, Asia, Africa, and the Americas testify to our product quality and trustworthiness.
Case Studies: Real-World Impact of HINADA Containerized MBR Systems
Industrial Park Wastewater Reuse
In a major industrial park in Southeast Asia, HINADA supplied a containerized MBR system with an integrated DAF system for pre-treatment. The result was a 98% reduction in pollutants, allowing the client to recycle over 80% of process water and achieve significant cost savings, while complying with all local and international discharge regulations.
Emergency Relief Operations
During a natural disaster in a remote region, our mobile MBR water treatment plant enabled rapid deployment of potable water treatment, serving thousands of people within a matter of days. The plug-and-play design and robust construction ensured trouble-free operation in adverse conditions.
Upgrading Municipal Wastewater Infrastructure
An urban municipality in Eastern Europe chose a series of HINADA modular MBR wastewater system units to replace outdated treatment facilities. The compact footprint allowed installation in space-constrained urban areas, while automated monitoring facilitated compliance and reduced staffing needs.
Frequently Asked Questions – Answered by HINADA Professionals
What is the typical lead time for a HINADA containerized MBR system? Most standard systems can be delivered within 8-12 weeks, with expedited options available for urgent projects.
What support does HINADA offer for system installation and commissioning? We provide full installation guidance, on-site or remote commissioning, and ongoing technical support.
How do HINADA systems handle fluctuating or high-strength wastewater? Our systems incorporate advanced process control and can be equipped with DAF system and robust membranes to accommodate variable influent loads.
Are spare parts and consumables readily available for international clients? Yes, we maintain a global logistics network to ensure fast delivery of critical components and consumables, including UF membrane modules and control electronics.
Why International Buyers Choose HINADA as Their Containerized MBR System Manufacturer
Discerning procurement professionals look for partners who deliver consistent quality, innovation, and value. HINADA distinguishes itself as a containerized MBR system manufacturer by offering:
Turnkey solutions tailored to project needs and local regulations.
Competitive pricing made possible by scale and manufacturing expertise.
Flexible financing and payment terms for international clients.
Comprehensive references from satisfied global customers.
Cutting-edge technology that sets new standards for water reuse and recycling.
Take the Next Step: Partner with HINADA for Your Water Recycling Needs
Whether you represent a municipal utility, an industrial conglomerate, a commercial developer, or an EPC contractor, HINADA Water Treatment Tech Co., Ltd. is ready to be your trusted partner. Our containerized MBR system and related solutions are the answer to the modern world’s water challenges—delivering reliability, performance, and sustainability. Contact our expert team today to discuss your project, request a tailored proposal, or schedule a factory visit. Join the global movement toward water resilience with HINADA, your gateway to advanced water recycling and purification.
Relevant Product Keywords Integrated:
containerized MBR system
MBR wastewater treatment plant
membrane bioreactor system
containerized MBR plant
industrial MBR system
modular MBR wastewater system
compact MBR system
containerized membrane bioreactor
mobile MBR water treatment plant
MBR package plant
containerized sewage treatment plant
portable MBR plant
DAF system
UF membrane module
containerized MBR system manufacturer
Choose HINADA for Sustainable, Reliable, and Innovative Water Treatment Solutions.