How Can a Water Treatment Plant in Food Industry Improve Filtration Efficiency
How Can a Water Treatment Plant in Food Industry Improve Filtration Efficiency
November 04, 2026
Author
Solution Provider, through a professional technical team, we provide customers with targeted equipment selection recommendations and comprehensive after-sales services, winning the trust and recognition of customers.
Sarah M.
The article presents a comprehensive, customer-oriented overview of how Hinada Water Treatment Tech Co., Ltd. (HINADA) enhances filtration efficiency in food industry water treatment plants. It details the integration of advanced membrane filtration systems, ultrafiltration membranes, reverse osmosis systems, automatic backwash filters, and water purification systems, all designed to meet the strict demands of food safety and operational efficiency. HINADA’s modular and turnkey solutions, supported by rigorous quality control and international certifications, enable food processors to minimize downtime, lower costs, and ensure regulatory compliance. The article also highlights the significance of after-sales support, energy efficiency, and digitalization (IoT monitoring) in modern water treatment. By addressing the core concerns of both technical and procurement professionals, HINADA positions itself as a trusted partner for serious buyers, offering proven, customizable, and future-ready solutions for water and industrial wastewater treatment in the food sector.
Introduction: The Importance of Advanced Filtration in Food Industry Water Treatment Plants
In the fast-evolving food processing sector, regulatory standards, sustainability expectations, and consumer demands for quality compel manufacturers to invest in advanced water treatment plant solutions. HINADA (Hinada Water Treatment Tech Co., Ltd.) stands at the forefront in providing next-generation water filtration, offering a wide spectrum of membrane filtration systems, industrial filtration equipment, ultrafiltration membranes, and reverse osmosis systems. This article explores how HINADA leverages cutting-edge water filtration plant technology to dramatically improve filtration efficiency, reliability, and cost-effectiveness for food industry clients, focusing on the most sought-after product keywords related to water treatment plant in food industry, water treatment for food processing, membrane filtration system, industrial water filtration, ultrafiltration membrane, reverse osmosis system, automatic backwash filter, water purification system, industrial wastewater treatment, water filter equipment, high-efficiency filtration, and more.
Key Challenges in Food Industry Water Treatment: The Need for Reliable Filtration
The food industry faces unique water treatment challenges: fluctuating feedwater quality, sensitive product safety requirements, strict discharge regulations, and the constant drive for higher operational efficiency. Conventional water filter equipment may not deliver the precision and reliability needed for this sector. HINADA addresses these pain points with membrane filtration systems, such as high-performance ultrafiltration membranes and reverse osmosis units, ensuring consistent removal of suspended solids, bacteria, viruses, and chemical contaminants. Genuine buyers prioritize solutions that minimize downtime, reduce maintenance, and guarantee compliance—a philosophy at the heart of HINADA's design and manufacturing process.
Membrane Filtration System: The Next Step in Water Treatment Plant Efficiency
HINADA's membrane filtration system technology represents a cornerstone for high-efficiency filtration in food industry water treatment plants. By integrating state-of-the-art hollow fiber ultrafiltration membranes and spiral-wound reverse osmosis systems, HINADA enables food processors to achieve:
Customizable configurations for diverse feedwater and process needs
End-buyers benefit from minimized production interruptions and lower operational costs, while procurement specialists appreciate HINADA's transparent cost structure and technical support.
Innovative Water Filter Equipment for Total Process Protection
HINADA has pioneered a portfolio of water filter equipment designed for scalability, ruggedness, and precise contaminant removal. Critical units include:
Automatic backwash filters: Self-cleaning, ideal for prefiltration, extend downstream membrane life
Cartridge and bag filter housings: Easy maintenance, available in sanitary-grade stainless steel
Industrial filtration equipment: Tailored for heavy loads, integrating seamlessly with existing CIP (Clean-in-Place) procedures
This approach ensures food processing water treatment plants run smoothly even with variable raw water quality, supporting both product integrity and regulatory compliance.
Reverse Osmosis System: Achieving Ultra-Pure Water for Food Processing
Reverse osmosis systems from HINADA deliver the highest purity water required for ingredient mixing, rinsing, and critical process steps. The advantages include:
Removal of dissolved salts, organics, and trace contaminants
Energy-efficient operation with advanced membrane materials
Integration with real-time monitoring and automatic control
Modular designs for easy expansion and retrofit
For procurement managers seeking reliable performance guarantees and low total cost of ownership, HINADA's reverse osmosis systems consistently outperform generic alternatives on the market.
Industrial Wastewater Treatment: Closing the Loop with Water Reuse
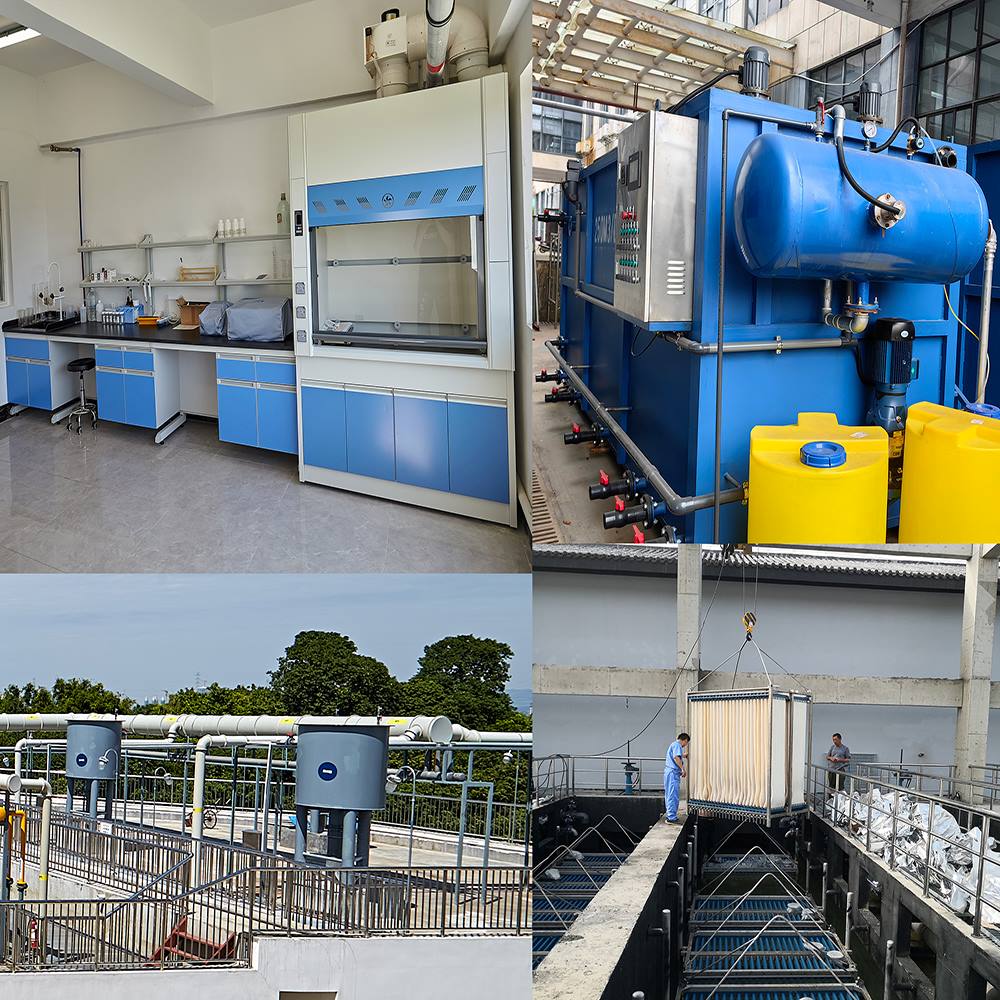
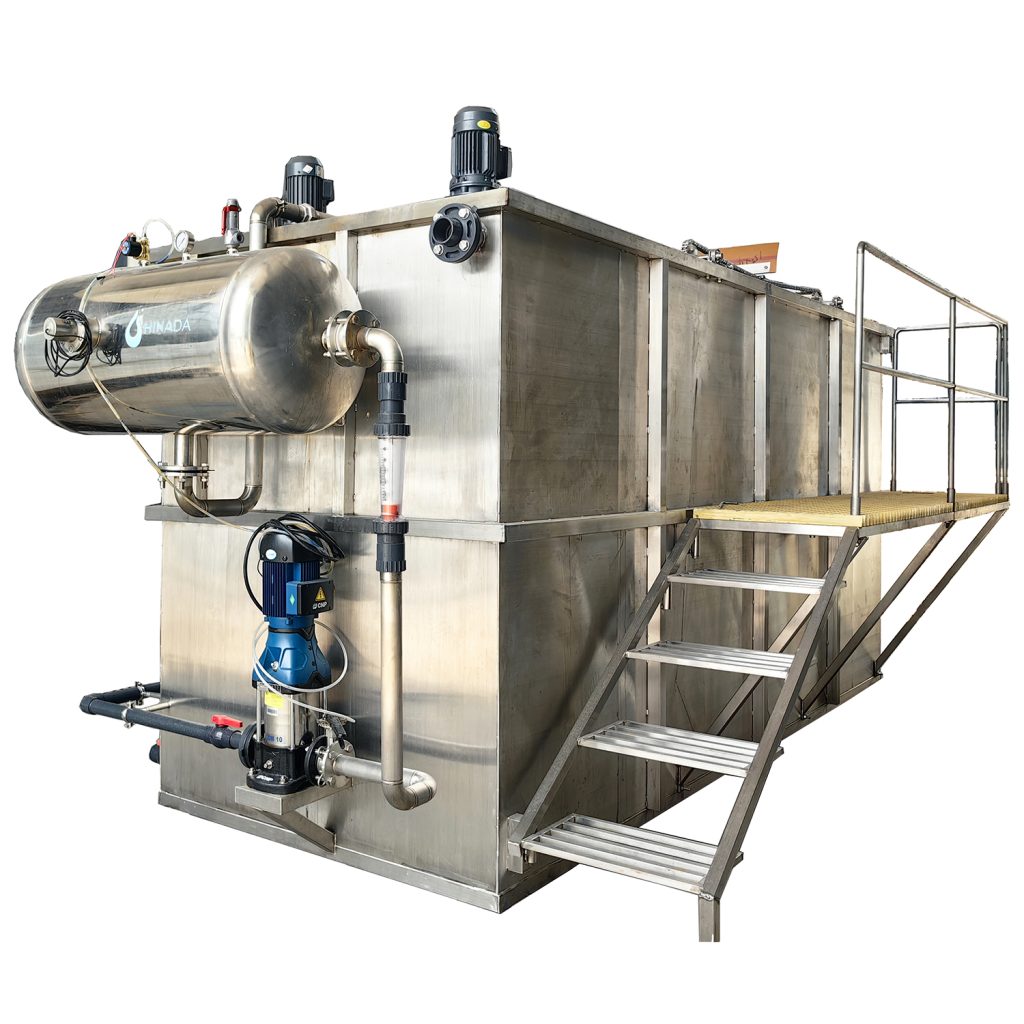
Water scarcity and stringent discharge limits drive the adoption of industrial wastewater treatment and water reuse technologies in the food sector. HINADA supplies advanced Wastewater Treatment Plants that combine dissolved air flotation, membrane bioreactor (MBR), and tertiary membrane filtration. These integrated systems enable food factories to:
Reduce freshwater intake and cut utility costs
Meet or exceed local and international discharge standards
Enable safe water recycling for non-potable applications
HINADA’s end-to-end engineering, rapid delivery, and expert commissioning make them the preferred choice among buyers seeking to future-proof their operations.
Automatic Backwash Filter: Enhancing System Autonomy and Reducing Labor
Labor costs and human error are perennial concerns for food processing facilities. The automatic backwash filter, a signature product from HINADA, automates the removal of accumulated solids from the filtration media without interrupting production. This technology:
Provides consistent filtration performance
Reduces operator intervention
Extends filter lifespan and reduces spare parts inventory
Procurement professionals value these benefits when comparing long-term operational costs and process dependability.
Water Purification System: Custom Solutions for Every Food Application
No two food processing operations are identical. HINADA offers modular water purification system designs, integrating ultrafiltration, activated carbon, and reverse osmosis, to match each client’s specific water quality and throughput demands. This solution-oriented philosophy ensures:
Faster project implementation
Optimized footprint and utility consumption
Scalable upgrades as production needs grow
From meat processing to beverage bottling, HINADA’s water purification systems empower buyers to realize fast returns on investment and long-term reliability.
HINADA’s high-efficiency filtration systems utilize advanced membrane materials and intelligent process controls. Key features include:
Superior solids capture with minimal pressure drop
Predictive maintenance alerts via IoT platforms
Optimized cleaning cycles to limit water and chemical usage
For decision-makers, these advantages translate into higher process yields, lower reject rates, and measurable sustainability gains—core motivators for capital equipment investments.
Technical Support, After-Sales Service, and Lifecycle Cost Optimization
Genuine buyers prioritize not only equipment performance but also the quality of technical support and after-sales service. HINADA’s team of process engineers and service technicians offer:
On-site commissioning, operator training, and SOP development
Remote diagnostics and troubleshooting
Spare parts logistics and maintenance planning
This comprehensive support ecosystem safeguards buyer investments and ensures uninterrupted plant operation, a critical factor in vendor selection for global food industry procurement teams.
Quality Control and Certifications: Meeting International Food Safety Standards
HINADA’s water treatment plant solutions for the food industry are manufactured under strict ISO 9001 quality standards and are compliant with food-grade material certifications (such as NSF and FDA). Validation documentation is provided for membrane filtration system and water purification system installations, ensuring audit readiness for multinational buyers.
Customization, Flexibility, and Turnkey Project Management
Food and beverage manufacturers are drawn to suppliers who can tailor solutions to local water chemistry, site constraints, and production schedules. HINADA’s project delivery model includes:
Comprehensive water analysis and pilot testing
3D plant layout design and detailed engineering
Turnkey installation and commissioning
This end-to-end approach shortens project timelines and reduces risks, offering tangible value to both technical and procurement stakeholders.
Energy Efficiency and Sustainability Integration
With energy costs rising, HINADA incorporates energy recovery devices and low-energy membrane options in reverse osmosis system and ultrafiltration membrane lines. Buyers committed to ESG (Environmental, Social, and Governance) principles benefit from reduced carbon footprints and enhanced resource stewardship.
Digitalization, IoT Monitoring, and Data-Driven Optimization
Modern food processing facilities require real-time oversight of filtration performance, water quality, and system health. HINADA equips water treatment for food processing installations with IoT-enabled sensors and cloud dashboards for:
Predictive maintenance and rapid issue resolution
Continuous regulatory compliance reporting
Insight-driven process improvements
Buyers thus gain unprecedented transparency, supporting both operational excellence and continuous improvement initiatives.
Global Reach, Local Expertise: HINADA’s International Food Industry Track Record
With reference projects spanning Asia, Europe, Africa, and the Americas, HINADA demonstrates global capability with local project execution. Multinational food industry buyers benefit from:
Consistent product quality and performance guarantees
Rapid response times and multilingual technical support
Flexible financing and export logistics management
This international network accelerates project delivery and assures buyers of ongoing support, regardless of location.
Case Studies: Delivering Value for Food Industry Leaders
HINADA’s installations in dairy, beverage, meat, and ready-to-eat sectors consistently achieve:
50%+ reduction in water and energy usage
99.99% pathogen rejection for ingredient water
Rapid payback periods (often under 24 months)
These proven, quantifiable results give buyers the confidence to invest in HINADA’s membrane filtration system and water purification system lines.
Integrating Disinfection and CIP: Total Water Treatment Plant Solutions
For comprehensive process security, HINADA also integrates UV disinfection, ozone, and chemical CIP (clean-in-place) systems into water treatment plant offerings. This ensures end-to-end protection from water intake to product filling, minimizing microbial risks and extending system service intervals.
FAQ: What Buyers Ask About Food Industry Water Treatment Solutions
Q: What is the expected lifecycle of HINADA’s ultrafiltration membranes and reverse osmosis systems? A: With proper maintenance and operation, ultrafiltration membranes typically last 5–7 years, and RO membranes up to 3–5 years, backed by a full warranty and global service network.
Q: How does HINADA ensure local regulatory compliance for water and wastewater discharge? A: All water treatment plant designs are engineered based on local standards, with validation and on-site testing to guarantee compliance. Customized documentation is provided for audits and certifications.
Procurement Insights: What Sets HINADA Apart for Serious Buyers?
Procurement professionals prioritize risk mitigation, total cost of ownership, and post-sale support. HINADA’s value proposition includes:
Transparent, detailed quotations with TCO modeling
Lifecycle support including upgrades, retrofits, and spare parts
Fast lead times and guaranteed delivery dates
Comprehensive after-sales technical service
These differentiators help procurement teams justify capital investments and build long-term supplier relationships.
Conclusion: The HINADA Advantage in Food Industry Water Treatment Plant Filtration Efficiency
HINADA (Hinada Water Treatment Tech Co., Ltd.) stands ready to support food industry buyers in achieving world-class water treatment plant performance, efficiency, and compliance. By integrating the latest in membrane filtration system, ultrafiltration membrane, reverse osmosis system, automatic backwash filter, water purification system, and industrial filtration equipment, HINADA delivers measurable ROI and future-proofs food production from water-related risks. Contact HINADA today to explore how your facility can benefit from the most advanced, reliable, and cost-effective water treatment solutions available.
Product Keywords Integrated in the Article:
Water treatment plant in food industry
Water treatment for food processing
Membrane filtration system
Industrial filtration equipment
Ultrafiltration membrane
Reverse osmosis system
Automatic backwash filter
Water purification system
Industrial wastewater treatment
Water filter equipment
High-efficiency filtration
Water filter for food industry
Food processing water treatment
Water purification plant
Water filtration plant
Industrial water filtration
Filtration system for food processing
Clean-in-place (CIP) system
Special integration of membrane filtration system and water purification system has been highlighted above in the context of advanced solutions for the food industry sector.