How Does Submerged Membrane Bioreactor Filtration Enhance Wastewater Treatment
How Does Submerged Membrane Bioreactor Filtration Enhance Wastewater Treatment
October 03, 2026
Author
Solution Provider, through a professional technical team, we provide customers with targeted equipment selection recommendations and comprehensive after-sales services, winning the trust and recognition of customers.
Sarah M.
Hinada Water Treatment Tech Co., Ltd. (HINADA) stands out as a leading Chinese manufacturer specializing in Submerged Membrane Bioreactor filtration systems, MBR ultrafiltration modules, and a comprehensive suite of membrane reactor products. HINADA’s advanced solutions seamlessly integrate biological treatment and membrane separation, offering buyers superior water quality, compact designs, and exceptional operational reliability. With a focus on buyers’ needs, the company provides modular, scalable, and energy-efficient systems suitable for industrial, municipal, and decentralized wastewater treatment. Their products, including hollow fiber membrane modules, flat sheet membrane elements, and integrated membrane reactors, deliver proven performance, longevity, and cost savings. HINADA’s expertise, technical support, and commitment to customization ensure that buyers receive tailored, high-value solutions for regulatory compliance, sustainability, and long-term operational excellence. Choosing HINADA means partnering with a trusted provider dedicated to advancing wastewater treatment through innovation and customer-centric service.
Introduction: The Need for Advanced Submerged Membrane Bioreactor Filtration in Modern Wastewater Treatment
In the rapidly evolving world of water treatment, industrial and municipal clients demand solutions that deliver not only compliance and sustainability, but also cost-effectiveness, operational flexibility, and high reliability. Hinada Water Treatment Tech Co., Ltd. (HINADA), a leading Chinese manufacturer, specializes in advanced submerged membrane bioreactor filtration systems, setting new standards in the field. Leveraging decades of experience, HINADA’s innovative range covers submerged membrane bioreactors, MBR ultrafiltration modules, hollow fiber membrane modules, submerged MBR filtration, membrane reactor systems, flat sheet membrane elements, MBR filtration systems, MBR membrane modules, and more. Our dedication to excellence makes us a strategic partner for genuine buyers seeking high-quality solutions for wastewater treatment challenges.
What Sets Submerged Membrane Bioreactor Filtration Apart?
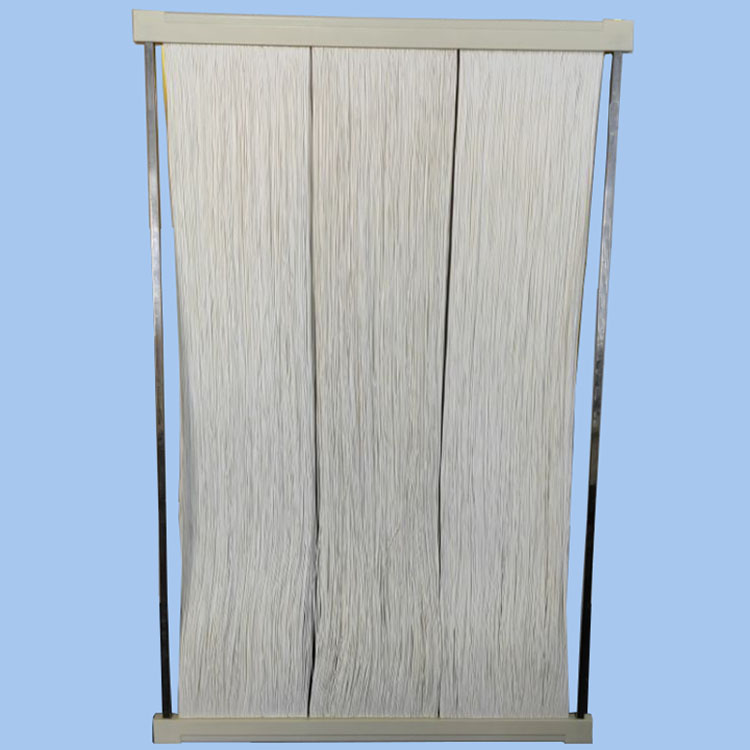
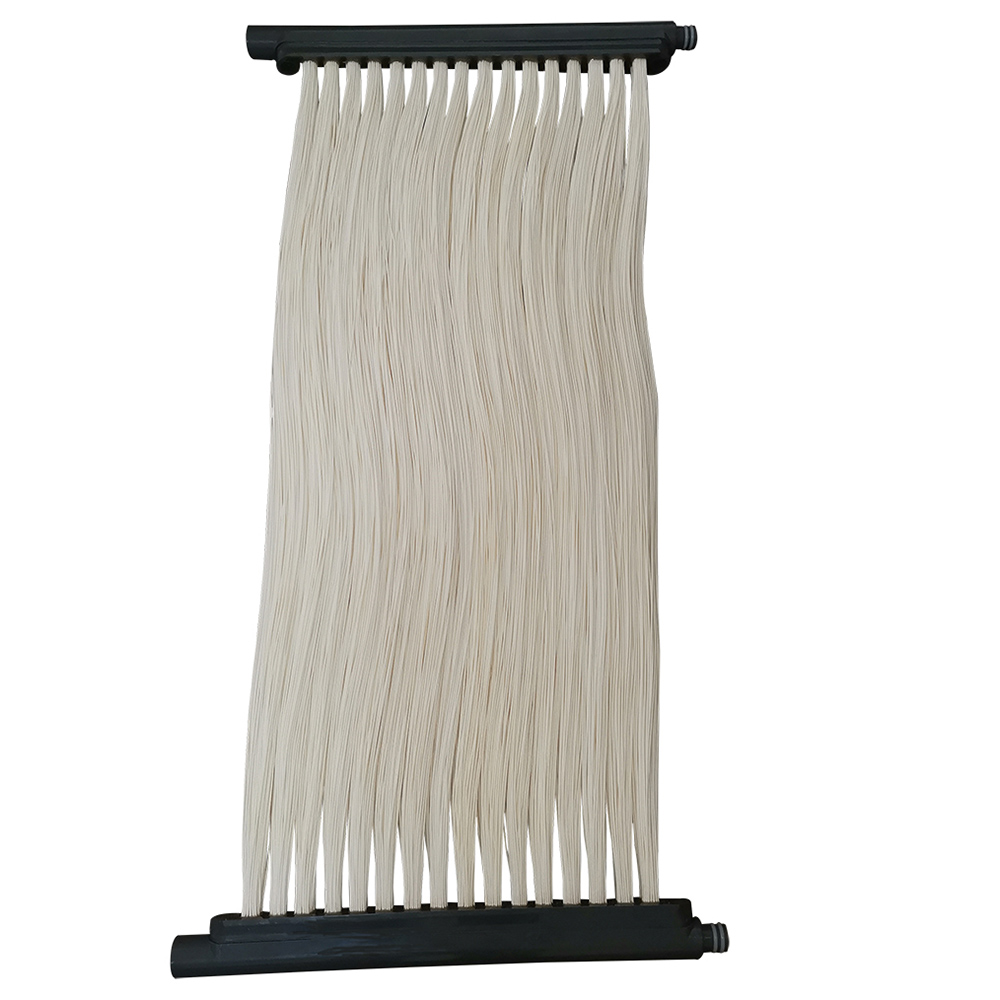
Submerged Membrane Bioreactor (MBR) Filtration combines a highly efficient biological treatment process with advanced physical separation, using robust membrane modules submerged directly in the bioreactor tank. This design eliminates the need for secondary clarifiers and tertiary filtration, delivering treated water of exceptional clarity and safety. HINADA’s full product suite—featuring submerged MBR filtration systems, MBR membrane modules, hollow fiber elements, and flat sheet membrane modules—caters to both municipal and industrial buyers who value consistent performance and reduced footprint.
HINADA Submerged Membrane Bioreactor Filtration: How It Works
HINADA’s submerged membrane bioreactor filtration systems are engineered to achieve superior results for a wide range of wastewater types. The process integrates biological degradation in the bioreactor with membrane separation, typically using hollow fiber membrane modules or flat sheet membrane elements. Wastewater enters the membrane reactor, where microorganisms break down organic contaminants. The mixed liquor is then filtered through submerged membranes, retaining solids and pathogens while allowing only clean water to pass through.
Our membrane bioreactor systems leverage MBR ultrafiltration technology, providing a physical barrier to bacteria and viruses. This high level of contaminant removal makes the treated water suitable for reuse, irrigation, or safe discharge, and meets the demands of buyers who require regulatory compliance and environmental responsibility.
Key Advantages for Strategic Buyers: Why Choose HINADA?
Compact System Design – HINADA’s integrated membrane reactor and compact MBR systems maximize space usage, ideal for retrofitting or limited installation space.
Superior Water Quality – Our advanced MBR technology consistently delivers effluent with low turbidity, low BOD/COD, and negligible suspended solids.
Operational Flexibility – Modular MBR filtration systems and membrane modules allow for easy capacity scaling and maintenance, reducing operational risk for buyers.
Energy Efficiency – Submerged MBR membrane modules minimize energy consumption through optimized aeration and advanced airflow distribution.
Longevity & Reliability – HINADA’s hollow fiber and flat sheet membranes offer outstanding chemical and mechanical durability, minimizing total cost of ownership.
Easy Automation & Monitoring – Our systems are designed for seamless integration with SCADA and IoT solutions, enabling predictive maintenance and remote control for peace of mind.
Product Portfolio: A Complete Range for Every Application
HINADA offers a comprehensive line of submerged membrane bioreactor filtration products, tailored to fit the unique needs of industrial, municipal, and commercial buyers:
Submerged MBR Filtration Systems – Turnkey solutions delivering robust performance for large-scale water reclamation and compact decentralized plants.
MBR Membrane Modules – Including both hollow fiber membrane modules and flat sheet membrane elements, suitable for new installations or retrofits.
MBR Ultrafiltration Units – Featuring advanced membrane materials and optimized module design for maximum flux and fouling resistance.
Integrated Membrane Reactors – Engineered to combine biological and physical treatment in a single, efficient process.
Industrial and Municipal MBR Systems – Customizable to meet various influent loads, regulations, and end-use requirements.
Application Scenarios: Meeting the Demands of Modern Buyers
With growing environmental regulations and water scarcity, buyers in sectors ranging from municipal wastewater facilities to food and beverage, pharmaceuticals, textiles, and chemical industries turn to HINADA for reliable membrane separation systems. Our proven solutions deliver:
Municipal Wastewater Reuse – Achieve consistent compliance and safe effluent for urban reuse.
Industrial Effluent Treatment – Remove difficult contaminants and enable closed-loop water recycling.
Decentralized Sewage Treatment – Compact, autonomous operation for rural communities, hotels, and resorts.
Greywater Recycling – Retrofit membrane reactor solutions for commercial buildings and residential complexes.
MBR Ultrafiltration and Membrane Reactor: Technology Highlights
HINADA’s MBR ultrafiltration units use advanced membrane materials and module configurations for maximum permeability and chemical resistance, ensuring stable operation even under fluctuating loads. Our membrane reactor systems are designed for seamless integration with existing infrastructure, and feature automated cleaning and monitoring, reducing operational costs and downtime for buyers focused on long-term investment value.
Our product research and development teams continually innovate in the areas of membrane anti-fouling, module compactness, and energy optimization—delivering future-proof solutions that stay ahead of regulatory and market trends.
Buyer’s Focus: What Experienced Procurement Professionals Value
Proven Track Record – HINADA has delivered thousands of submerged membrane bioreactor filtration and MBR membrane module units domestically and overseas.
Full Technical Support – We offer bilingual technical documentation, on-site commissioning, and responsive after-sales service—crucial for seamless project execution.
Flexible Customization – Whether upgrading an existing membrane separation system or specifying for a new facility, HINADA provides tailored designs with rapid production cycles.
Transparent Quality Assurance – Our products are manufactured under strict ISO and CE certifications, with traceable QC at every step.
Cost-Competitive Solutions – Direct-from-manufacturer pricing, consolidated shipping, and long membrane lifespans help buyers maximize ROI.
Making the Right Choice: How HINADA Supports Genuine Buyers
As a leading Chinese manufacturer, HINADA’s reputation is built on trust, reliability, and technical leadership. For buyers seeking to invest in submerged membrane bioreactor filtration technology, selecting a partner with proven expertise and manufacturing scale is vital. We support procurement with detailed membrane performance data, references from successful installations, pilot program capabilities, and flexible commercial terms. Our team understands that buyers seek more than just equipment—they demand solutions that safeguard their operations, reputation, and future growth.
Long-Term Benefits of HINADA’s Submerged Membrane Bioreactor Filtration Solutions
Regulatory Compliance – Reliable removal of pathogens and contaminants secures permits and minimizes liability.
Lower Lifecycle Costs – High-efficiency design and durable membranes reduce energy and replacement costs.
Water Reuse & Sustainability – Enable clients to achieve sustainability targets and tap into new revenue streams from reclaimed water.
Conclusion: Partner with HINADA for Next-Generation Wastewater Treatment
For genuine buyers and procurement professionals, investing in HINADA’s submerged membrane bioreactor filtration technology is the smart choice for modern, efficient, and future-ready wastewater treatment. Our comprehensive portfolio—from MBR ultrafiltration modules to integrated membrane reactors—empowers clients to achieve regulatory compliance, operational excellence, and sustainability at scale. Contact our technical team today to discover how HINADA can help you meet your wastewater treatment challenges—efficiently, reliably, and cost-effectively.