Containerized MBR System Solutions for Compact Installation
Containerized MBR System Solutions for Compact Installation
October 20, 2026
Author
Solution Provider, through a professional technical team, we provide customers with targeted equipment selection recommendations and comprehensive after-sales services, winning the trust and recognition of customers.
Sarah M.
Hinada Water Treatment Tech Co., Ltd. (HINADA) is a leading Chinese manufacturer specializing in containerized MBR system solutions for compact installation. Their innovative products integrate advanced membrane bioreactor (MBR) technology into ISO containers, offering highly modular, plug-and-play solutions for municipal, industrial, and decentralized wastewater applications worldwide. HINADA’s containerized MBR systems are designed for rapid deployment, space savings, robust operation, and superior effluent quality, supporting water reuse and green sustainability goals. Buyers benefit from direct manufacturer pricing, international certifications, turnkey delivery, and full-cycle technical support, ensuring rapid return on investment and compliance with stringent regulatory standards. The systems are ideal for remote, mobile, and constrained environments, including mining camps, construction sites, tourism resorts, and disaster relief operations. With a strong export track record, proven membrane technology, and deep understanding of customer needs, HINADA empowers buyers to achieve reliable, efficient, and sustainable wastewater treatment. For project-specific inquiries and solutions, HINADA stands ready as your trusted partner in containerized MBR technology.
In today's rapidly urbanizing and industrializing world, the demand for efficient, space-saving, and cost-effective wastewater treatment solutions has never been greater. Hinada Water Treatment Tech Co., Ltd. (hereafter referred to as HINADA), a leading Chinese manufacturer, specializes in containerized MBR system solutions for compact installation, offering robust, turnkey, and highly modular solutions that address the unique needs of municipal, industrial, and decentralized clients worldwide.
Product Overview: Containerized MBR System Solutions for Compact Installation
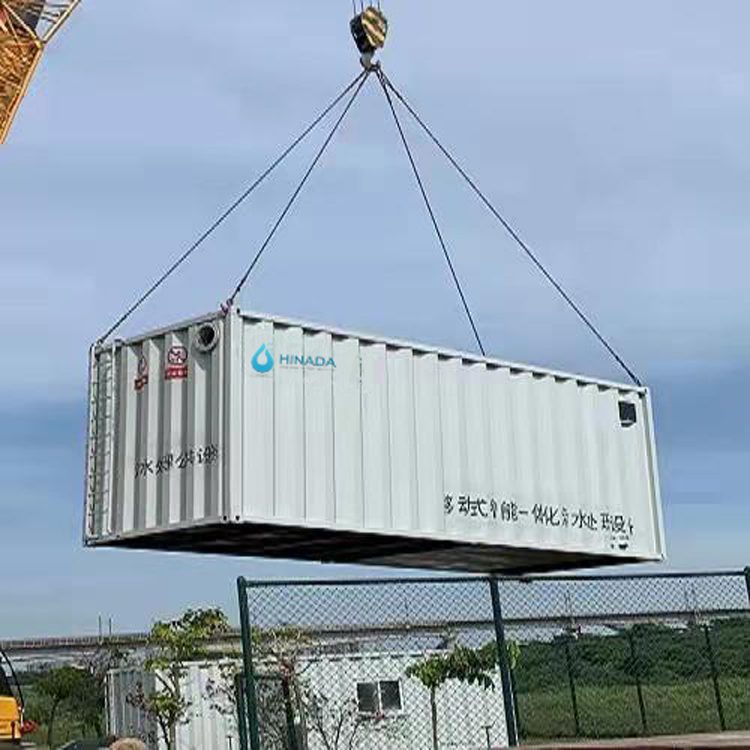
HINADA’s containerized MBR system solutions for compact installation integrate cutting-edge Membrane Bioreactor (MBR) technology into robust ISO shipping containers, providing high-efficiency biological treatment and advanced membrane filtration within a single, transportable package. The main product keywords covered in this article include:
containerized MBR system
compact wastewater treatment plant
modular MBR solutions
plug and play MBR system
mobile sewage treatment
decentralized wastewater treatment
integrated MBR unit
prefabricated MBR plant
turnkey containerized MBR
energy-efficient MBR solution
high-efficiency membrane filtration
industrial wastewater MBR system
municipal compact MBR
advanced water reuse system
portable MBR container
remote site sewage treatment
HINADA leverages over a decade of expertise in the field, with thousands of successful installations worldwide, supporting clients in sectors such as municipal sewage, food & beverage, pharmaceuticals, textiles, and remote mining camps.
Key Features and Advantages of HINADA’s Containerized MBR Solutions
1. Space-Saving, Flexible Design
The compact footprint and modular design of HINADA’s containerized MBR systems allow for deployment in space-restricted and challenging environments. Clients can expand capacity simply by adding more container modules in parallel or series, eliminating the need for large civil works or permanent infrastructure.
2. Rapid Deployment and Plug-and-Play Operation
Each containerized MBR system is prefabricated and factory-tested, ensuring rapid delivery and start-up. HINADA’s plug-and-play MBR solutions can be operational within hours of arrival onsite, minimizing downtime and construction costs for buyers pursuing fast-track projects or emergency relief.
HINADA’s containerized MBR units are built with corrosion-resistant materials, reinforced containers, and quality components, designed for reliable long-term operation even in harsh environments. The systems are ideal for both permanent and temporary installations, offering flexibility for seasonal or project-based demands.
4. Advanced Membrane Filtration and High-Quality Effluent
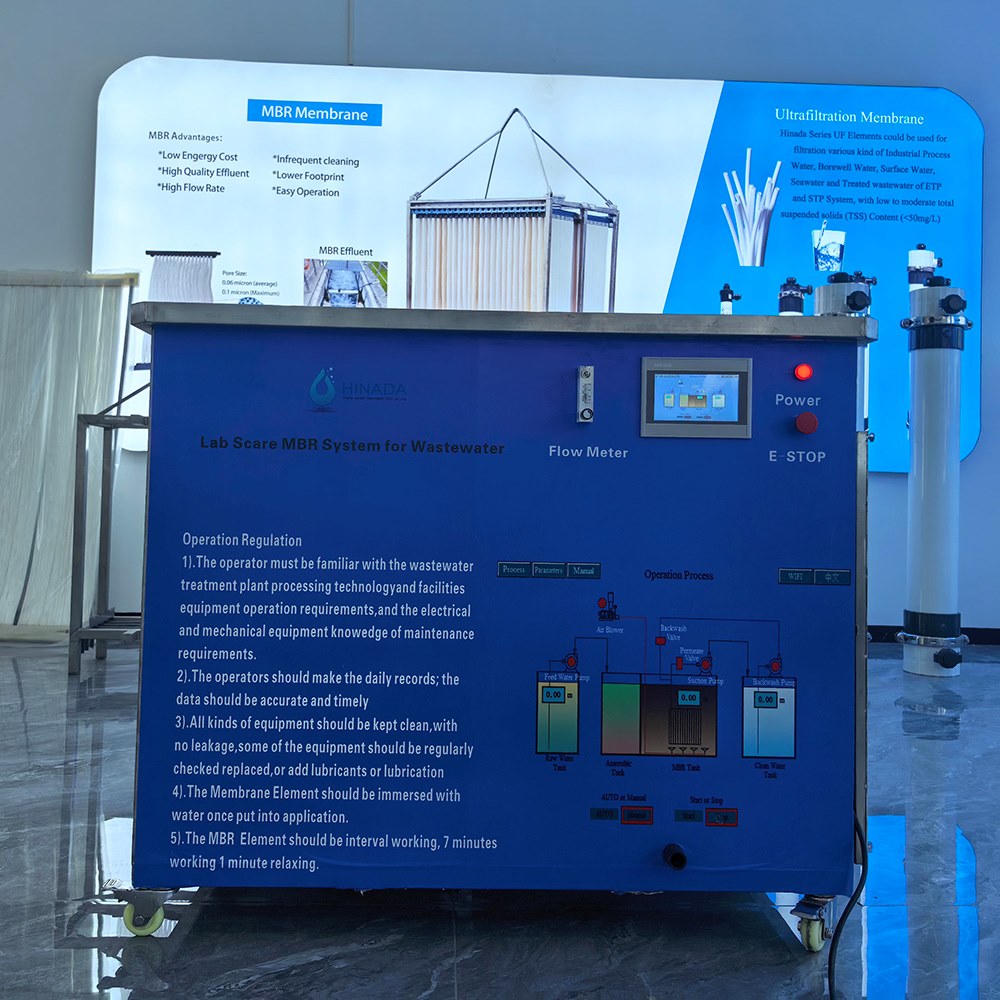
Utilizing state-of-the-art hollow fiber or flat sheet membranes, HINADA’s MBR systems achieve superior solids-liquid separation, producing effluent suitable for direct discharge, irrigation, or advanced reuse. This closes the water loop for clients with stringent regulatory requirements or water scarcity challenges.
5. Energy-Efficient and Low Maintenance
With optimized aeration control, energy-efficient blowers, automatic backwashing, and smart PLC-based system management, HINADA delivers MBR solutions with minimized operational costs and labor requirements, driving long-term buyer satisfaction and return on investment.
6. Integrated Remote Monitoring and Control
For enhanced reliability and transparency, HINADA offers optional IoT-based remote operation and real-time monitoring, empowering clients to manage multiple installations from a central location and receive proactive maintenance alerts.
Applications of Containerized MBR Systems: Addressing Diverse Client Needs
The broad adaptability of HINADA’s containerized MBR solutions makes them the preferred choice for:
Municipal wastewater treatment in dense urban locations
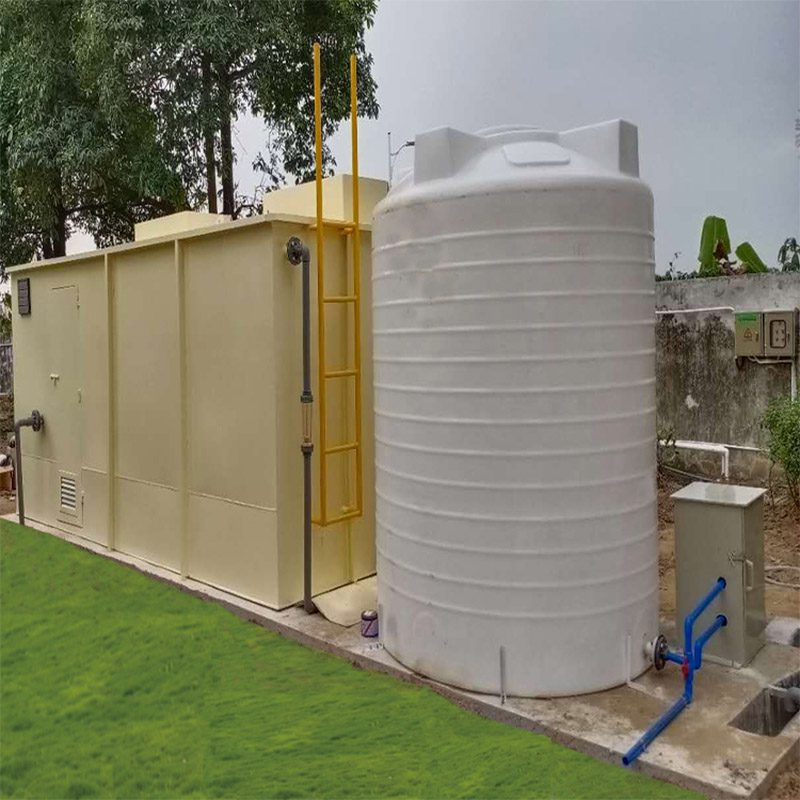
Industrial effluent treatment at remote or temporary sites
Camp and construction site sewage management
Decentralized and rural community sanitation
Tourism resorts and eco-lodges
Disaster relief and emergency sanitation
In each case, buyers benefit from the mobility, scalability, and compliance assurance that HINADA’s containerized MBR technology offers.
Buyer’s Perspective: Why Choose HINADA as Your MBR System Partner?
1. Manufacturer Direct – Quality at Competitive Prices
As a true manufacturer, HINADA controls every stage of design, fabrication, and quality control. This guarantees buyers consistent quality, rapid customization, and competitive pricing without middleman markups. For procurement professionals, this translates into lower risks and higher transparency throughout the project lifecycle.
2. Proven Export Experience and International Certifications
HINADA’s products are widely exported to markets in Europe, Asia, Africa, South America, and the Middle East. All containerized MBR units are manufactured in accordance with ISO standards, and can be supplied with CE certification and local compliance documentation as required. This facilitates import procedures and project approvals for global clients.
3. One-Stop Customization and Technical Support
From initial concept and process design, through to delivery, installation, and after-sales service, HINADA provides full-cycle technical support. Customizations can include container size (10ft/20ft/40ft), treatment capacity, process configuration (MBR, MBBR, SBR), and advanced automation options, ensuring your solution precisely matches your project requirements.
4. Turnkey Solutions for Rapid ROI
HINADA’s turnkey approach minimizes the time and resources buyers need to commit, providing a fully integrated, factory-assembled system that arrives ready to connect and operate. This is particularly attractive for investors, contractors, and end-users seeking fast-track project execution and rapid return on investment.
Professional Insights: Understanding Buyer Motivation and Project Success Factors
As technical and procurement professionals know, purchasing a containerized MBR system is about more than just equipment supply. Buyers seek assurance of process performance, regulatory compliance, operational reliability, and lifecycle cost-effectiveness. HINADA recognizes these pain points and delivers solutions that:
Minimize total cost of ownership through energy savings, long membrane life, and low maintenance
Provide robust documentation and after-sales support for installation, commissioning, and operator training
Offer flexible financing, shipping, and warranty options tailored to international buyers
Leverage local partnerships for installation and service if required
For customers in water-scarce regions or industries with strict environmental oversight, choosing a proven Chinese manufacturer like HINADA also means leveraging global supply chain strengths and leading membrane technology, all at highly competitive costs.
Integration of Key Industry Trends: Water Reuse and Green Sustainability
With global trends pointing toward water reuse and the imperative for compact, low-carbon wastewater treatment, HINADA’s containerized MBR solutions offer a forward-looking answer. The ability to recycle treated effluent on-site supports sustainability goals, reduces freshwater demand, and enhances project value for environmentally conscious buyers. Furthermore, the modular system can be relocated or upsized as needs evolve, ensuring long-term adaptability.
Case Study: HINADA Containerized MBR Success in Remote Mining Camp
In 2023, HINADA supplied a 100m3/day containerized MBR system to a mining camp in Central Asia. Facing extreme temperatures, rugged terrain, and tight construction timelines, the client required a robust, mobile, and hassle-free wastewater solution. HINADA’s prefabricated, insulated and automated MBR container was delivered, installed, and commissioned within 14 days. The system consistently meets discharge standards for reuse in dust suppression and irrigation, exemplifying the reliability and convenience of HINADA’s modular MBR technology.
FAQs: Key Buyer Questions Answered
How fast can HINADA deliver a containerized MBR unit?
Standard units can be ready for shipment within 4-8 weeks after order confirmation, while customized systems may require slightly longer. All units are factory-assembled, minimizing onsite work.
What is the typical lifespan of an MBR membrane?
With proper operation and maintenance, HINADA’s high-quality membranes typically last 5-8 years, supported by local service partners and global logistics for replacements.
Can HINADA’s containerized systems handle high-load industrial waste?
Yes, systems can be engineered for high-strength industrial effluents, with optional pre-treatment and advanced process control to ensure stable performance.
Contact HINADA: Your Trusted Partner for Containerized MBR System Solutions
Choosing the right technology partner is critical to project success. With HINADA, buyers are assured of top-tier containerized MBR system solutions for compact installation, engineered for flexibility, efficiency, and long-term value. For inquiries, technical consultation, or to request a detailed proposal, contact HINADA Water Treatment Tech Co., Ltd. today and discover the future of sustainable, containerized wastewater treatment.
Keywords integrated in this article: containerized MBR system, compact wastewater treatment plant, modular MBR solutions, plug and play MBR system, mobile sewage treatment, decentralized wastewater treatment, integrated MBR unit, prefabricated MBR plant, turnkey containerized MBR, energy-efficient MBR solution, high-efficiency membrane filtration, industrial wastewater MBR system, municipal compact MBR, advanced water reuse system, portable MBR container, remote site sewage treatment, water reuse, compact low-carbon wastewater treatment.